
Picking the right steel for your injection mold base can feel overwhelming, can’t it? There are so many grades, and making the wrong choice means spending too much or ending up with a base that wears out or fails prematurely. Let’s cut through the confusion.
The best steel depends on the application: standard bases often use cost-effective, machinable carbon steels like S50C/10451, while more demanding bases benefit from pre-hardened P202. High-wear cavity/core inserts require dedicated tool steels like H13 or S1363, selected for hardness and polishability.
Separate the mold-base specification from the requirements of cavity, core and wear components. Review the actual plate geometry, support, load, corrosion exposure and specified steel condition before comparing material options.
What Steel Do We Typically Use for the Mold Base Itself?
It’s easy to get lost in steel designations, right? You hear about H13, S136, P20… but do all these apply to the main structure, the mold base plates? Using super-hard tool steel for the entire base would be incredibly expensive and difficult to machine. So, what’s actually used?
Mold base plates4 (like the A-plate, B-plate, support plates) are typically made from medium-carbon steels5 such as S50C (Japan standard) or AISI 1045/1050 (US standard). For higher requirements, pre-hardened P20 steel is also a common choice for base plates, offering more strength.
The key is understanding the function of the mold base plates versus the cavity and core inserts. The base plates provide the main structural support for the mold. They hold everything together, align the two halves, contain the ejector system, and provide mounting points for the machine. Their primary requirements are:
- Sufficient Strength and Rigidity: To withstand clamping forces and injection pressures without significant deflection. Deflection leads to flash and dimensional instability.
- Good Machinability: Base plates need extensive machining for pockets to house inserts, channels for cooling, holes for leader pins, bushings, ejector pins, bolts, etc. Ease of machining keeps costs down.
- Dimensional Stability: The material should remain stable after machining and during operation.
- Cost-Effectiveness: Since base plates make up a large volume of the mold, using an economical material is important.
This contrasts sharply with cavity and core inserts, which directly shape the plastic. Their needs focus on: - High Hardness and Wear Resistance: To withstand the abrasion and pressure of flowing plastic over many cycles.
- Good Polishability: For achieving the desired surface finish on the part.
- Corrosion Resistance: Especially important for certain plastics like PVC.
-
Thermal Conductivity: To facilitate efficient cooling.
Because these requirements differ significantly, we use different steels:Feature Mold Base Plates (e.g., S50C, P20) Cavity/Core Inserts (e.g., H13, S136) Primary Role Structural Support, Housing Shaping Plastic, Wear Surface Key Needs Strength, Machinability, Cost Hardness, Wear Resistance, Polishability Typical Steel Medium Carbon, Pre-Hardened Alloy Tool Steel (often requires hardening) Hardness ~18-32 HRC ~48-55+ HRC (after heat treatment) Early in my career, I saw a project where someone specified H13 for the entire mold, base plates included. The machining time and cost were astronomical, and the potential for warping during heat treatment of those large plates was a nightmare. It taught me the crucial lesson: use the right steel for the right job. The base needs a solid foundation material, not necessarily the hardest material.
S50C and Equivalents: The Standard Choice for Mold Bases?
You need a reliable, cost-effective material for the bulk of your mold structure, don’t you? Using specialized, expensive steels for standard base plates often doesn’t make economic sense if a more common grade works perfectly well. So, what’s the go-to option?
S50C and related medium-carbon grade designations such as AISI/SAE 1045 or 1050 and C45/C50 are medium-carbon steels commonly used for standard mold bases. They offer a good balance of strength, toughness, excellent machinability, and cost-effectiveness, making them ideal for the structural components of many molds.
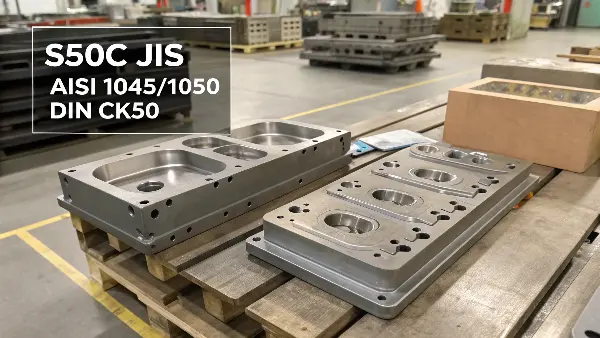
Think of S50C and its close relatives as the workhorses of the mold base world. Let’s break down why they are so frequently used:
- Composition and Properties: These are medium-carbon steels, typically containing around 0.45% to 0.55% carbon. This gives them decent strength and hardness (with hardness specified in the actual delivery condition; do not treat a low-range HRC value and an HB range as interchangeable acceptance criteria) right out of the box, without needing heat treatment for base plate applications. This hardness level provides good structural integrity but is still very easy to machine.
- Excellent Machinability: This is a major advantage. Mold bases require significant milling, drilling, tapping, and grinding to create pockets for inserts, cooling lines, ejector pin holes, guide pin holes, etc. The ease with which S50C/1045 can be machined translates directly into faster production times and lower manufacturing costs. At CKMOLD, our machinists appreciate working with these materials for standard bases.
- Cost-Effectiveness: Compared to alloy tool steels, these carbon steels are significantly less expensive. Since the base plates constitute a large portion of the mold’s weight and volume, using a cost-effective material here helps manage the overall mold budget effectively.
-
Equivalents: Steel standards vary globally. The following are related grade families, not automatic substitutions. Compare the governing standard, chemistry, delivery condition, section size and required properties before approving a replacement:
Standard Common Grade(s) Notes JIS S50C, S55C Japanese Standard AISI/SAE 1045, 1050 US Standard DIN C45, CK45, C50 German Standard GB 45#, 50# Chinese Standard - Limitations: While great for general purposes, S50C/1045 isn’t intended for high-wear surfaces or direct forming of plastic parts (unless it’s a very low-volume prototype). Its hardness isn’t sufficient for long production runs against abrasive plastics, and it won’t hold a high polish like dedicated cavity steels. Its strength is good, but for very large bases or extremely high injection pressures, deflection might become a concern, potentially leading designers like Jacky to consider P20.
In summary, S50C and related, separately approved grades can provide the reliable, machinable, and affordable foundation needed for a vast majority of injection mold bases.When Should You Consider Upgrading to P20 Steel for Your Mold Base?
While standard carbon steel works for many bases, sometimes you need something more robust, right? Perhaps the mold is very large, will endure long production runs, or handles higher injection pressures. Simply sticking with S50C might risk deflection or wear over time. When does it pay to upgrade the base material?
Consider upgrading to P20 steel for mold base plates when you need higher strength and rigidity6 (e.g., for large molds, high pressures), better wear resistance7 for longer mold life, or if simple forming features or runner gates are machined directly into the base plates.
P20 is a very common and versatile mold steel, often used for cavities and cores in medium-volume molds, but it also finds significant use in mold bases, particularly the main A and B plates (cavity and core retainer plates). Here’s why and when you’d choose it over S50C/1045 for the base:
- What is P20? P20 is an alloy tool steel, typically containing chromium and molybdenum. It’s supplied in a pre-hardened condition, usually around 28-32 HRC. This means it doesn’t require heat treatment after machining for most applications, saving time and avoiding distortion risks associated with hardening large plates.
- Increased Strength and Rigidity: P20 in a specified prehardened condition can offer different strength and wear properties from a nominated carbon-steel condition. Higher hardness does not by itself establish a large increase in elastic rigidity; compare Young’s modulus and the plate/support geometry separately. This is crucial for very large mold bases where the span between supports is greater, or in molds subjected to high injection pressures. Check elastic plate deflection using the actual modulus, support span, plate thickness, pockets and pressure load. A steel substitution alone does not ensure adequate seal-off or dimensional accuracy. A stronger steel is not a substitute for checking plate deflection and the support arrangement.
- Enhanced Wear Resistance: The higher hardness of P20 provides better resistance to wear and tear compared to standard carbon steels. This applies to wear from handling, clamping, and potentially from the operation of mold components like leader pins or interlocks over long production runs. It contributes to a longer overall lifespan for the mold base.
- Suitability for Machined Features: If simple runner systems, gates, or even some non-critical forming features are machined directly into the A or B plate (instead of using separate inserts), P20’s better wear resistance makes it a more suitable choice than S50C. It can withstand the flow of plastic better, especially near gate areas.
- Trade-offs: The main drawbacks of using P20 for base plates are increased material cost and slightly more difficult/slower machining compared to S50C/1045. You need to weigh these factors against the performance benefits. Often, it’s a cost-benefit analysis: is the higher initial cost justified by the need for increased strength, longer life, or direct machining of features? At CKMOLD, we often recommend P20 for bases destined for high-volume production or for larger, more complex tools.
P20 vs. H13: Why Aren’t Cavity Steels Used for the Whole Base?
You might hear P20 mentioned for both bases and cavities, and then hear about H13 primarily for cavities. This can be confusing. If H13 is so good for cavities, why don’t we just use it for the entire mold base for maximum durability? The answer lies in balancing properties, cost, and manufacturability.
P20 is a pre-hardened steel (~30 HRC) offering good machinability, used for bases or medium-wear cavities. H13 is a hot-work tool steel that requires heat treatment to achieve high hardness (~48+ HRC) for excellent wear/heat resistance in demanding cavities/cores. Using H13 for bases is usually cost-prohibitive and impractical.
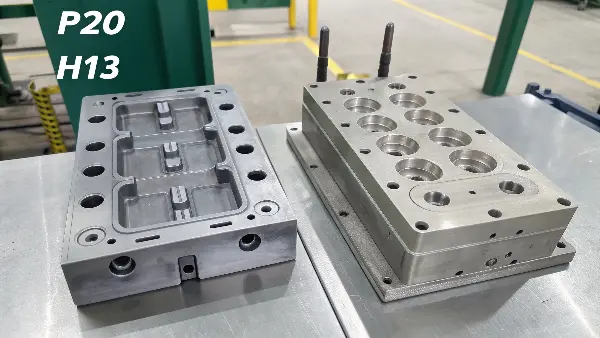
Understanding the fundamental differences between P20 and H13 clarifies why they are used in distinct roles within a mold:
- P20 Deep Dive:
- Type: Pre-hardened alloy steel (Chromium-Molybdenum).
- Hardness: Supplied typically 28-32 HRC. Ready to machine.
- Primary Use: Mold bases (especially higher quality), large inserts, medium-wear cavities/cores for moderate production volumes.
- Machinability: Good, significantly easier than fully hardened tool steels.
- Heat Treatment: Generally not required after machining (it’s already pre-hardened). Can be through-hardened further, but less common for base applications.
- Cost: Moderate. More expensive than S50C, less expensive than H13.
- H13 Deep Dive:
- Type: Hot-work tool steel (Chromium-Molybdenum-Vanadium).
- Hardness: Supplied soft (~20 HRC), requires heat treatment (quenching and tempering) after machining to reach working hardness of ~48-52 HRC.
- Primary Use: High-wear cavities and cores, components requiring high toughness and heat resistance (die casting dies too).
- Machinability: Relatively easy in the soft state, much more difficult after hardening. Often requires EDM or grinding post-hardening.
- Heat Treatment: Mandatory after machining to achieve desired properties. This process carries risks of distortion or cracking, especially on large, complex parts.
- Cost: Higher than P20.
Why Not H13 for Bases?- Cost: H13 material is significantly more expensive than P20 or S50C. Using it for large base plates would drastically increase the mold cost unnecessarily.
- Machinability: While machinable in its soft state, the sheer volume of machining required for a base plate would still be costly. Post-hardening machining is very slow and expensive.
- Heat Treatment: Hardening large, thick base plates uniformly and without distortion is extremely challenging and risky. The potential for warping or cracking is high, potentially ruining the entire plate.
- Overkill: The extreme wear resistance and heat resistance of H13 are simply not needed for the structural support function of a base plate. P20 or even S50C provides sufficient strength and durability for this role.
Using H13 for the base would be like building a house foundation out of surgical-grade stainless steel – incredibly expensive and offering no practical advantage over high-strength concrete. It’s about using the appropriately engineered material for each specific function. We reserve H13 and similar high-performance tool steels (like S136 for corrosion resistance) for the inserts that do the heavy lifting of forming the plastic part.So, How Do You Choose the ‘Best’ Steel for Your Specific Mold?
With several options for bases (S50C, P20) and many more for cavities (P20, H13, S136, etc.), how do you make the final call? There isn’t one single ‘best’ steel; it’s about making the most appropriate choice based on the project’s specific needs and constraints. Getting this wrong means either overspending or facing premature failure.
The ‘best’ steel choice involves balancing factors: component type (base vs. cavity), expected production volume/mold life, part material abrasiveness, required surface finish, structural demands (size, pressure), and budget. Match the steel’s properties to these requirements for optimal performance and cost.
Select the base material by reviewing the load, support geometry, machining and maintenance requirements together. Use the actual producer’s grade and supply condition rather than treating a familiar steel label as a complete specification.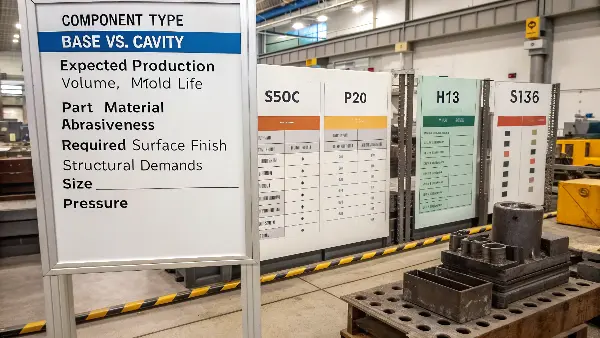
- Identify the Component: Is it a mold base plate (A, B, support, ejector housing) or a cavity/core insert? This is the first and most crucial split.
- Base Plates: Focus on structural integrity, machinability, stability, cost. Main candidates: S50C/1045, P20.
- Cavity/Core Inserts: Focus on wear resistance, hardness, polishability, toughness, corrosion resistance (if needed). Main candidates: P20 (lower volume/wear), H13 (high volume/wear), S136 (corrosion/polish), and other tool steels.
- Estimate Production Volume & Required Mold Life:
- Low Volume / Prototype: S50C base is likely sufficient. Inserts could be P20, aluminum, or even S50C if very low volume.
- Medium Volume (e.g., 50k – 500k shots): P20 base often preferred for better durability. P20 inserts might suffice, or H13 for moderate wear resistance.
- High Volume (e.g., 1M+ shots): P20 base strongly recommended, or even higher grades in some extreme cases. H13 or other high-wear resistant tool steels (e.g., PM steels) essential for cavities/cores.
- Consider Part Material: Is the plastic abrasive (e.g., glass-filled nylon)? Or corrosive (e.g., PVC)?
- Abrasive Materials: Demand higher hardness/wear resistance for cavities/cores (a wear-resistance specification based on the filler, contact mechanism and replaceable components). Might favor P20 base over S50C for slightly better wear on guiding elements.
- Corrosive Materials: Requires corrosion-resistant insert steel like S136 (stainless). Base material choice is less critical unless fumes are extreme.
- Evaluate Structural Demands:
- Large Mold Base Size: Increases risk of deflection. Check support layout, section stiffness and the actual elastic modulus; do not infer substantially lower deflection from P20 hardness alone.
- High Injection Pressure: Also increases deflection risk, favouring P20 for base plates.
- Define Surface Finish Requirements:
- High Polish / Optical: Requires specific insert steels (e.g., S136, NAK80) capable of achieving and holding a mirror finish. Base material doesn’t directly impact part finish.
- Factor in the Budget: There’s always a cost trade-off.
- S50C Base < P20 Base
- P20 Insert < H13 Insert < S136 Insert < Powder Metallurgy Steels
Balancing these factors leads to the optimal choice. For many of Jacky’s consumer electronic parts (potentially high volume, good finish), a P20 base with H13 or S136 inserts would be a common and solid specification. A simpler industrial part with lower volume might be perfectly fine with an S50C base and P20 inserts. Talking through these factors with your mold maker is always a good idea – a project review should compare the specified components, material certificates and structural calculations.Separate Elastic Deflection, Strength and Wear in the Mold-Base Review
These are three different checks. Elastic stiffness depends on material modulus and geometry; strength concerns yielding or failure; wear concerns contact surfaces and operating conditions. In a simplified rectangular beam with the same load, span and width, bending stiffness scales with E × thickness cubed. Increasing thickness by 20% gives 1.728 times the section stiffness before pocket, support and three-dimensional effects are considered. This is an illustrative comparison, not a mold-plate design calculation.
Specify plate dimensions and pockets, unsupported spans, support pillars, cavity-pressure loading, assembly preload, delivery condition and material certification. Assess elastic deflection and strength separately. MISUMI’s mold-rigidity tutorial explains the role of E × I; a harder steel name is not a substitute for that review.
What Should a Mold-Base Quotation Identify?
Request component-level steel designation, supplier/standard, delivery hardness, plate and support layout, critical fits and the substitution approval process. Keep base support design distinct from cavity and core steel selection. Send the mold-base requirements for engineering review and email the assembly and machine-interface drawings to jerry@ckmold.com.
Conclusion
Selecting the right steel for your mold base and inserts is a critical decision impacting cost, performance, and longevity. Use S50C/1045 for standard bases, consider P20 for higher demands, and choose appropriate tool steels like H13 or S136 for the cavities/cores based on project specifics.
-
Explore this link to understand the applications and benefits of S50C/1045 steel in mold making, ensuring you make an informed choice. ↩
-
Discover the unique properties of pre-hardened P20 steel and why it’s favored for demanding mold applications, enhancing your design decisions. ↩
-
Learn about the characteristics of H13 and S136 tool steels to choose the right material for high-wear applications in mold design. ↩
-
Understanding the materials used for mold base plates is crucial for effective design and manufacturing processes. ↩
-
Exploring the applications of medium-carbon steels can enhance your knowledge of their role in various industries. ↩
-
Understanding the significance of strength and rigidity can help you make informed decisions for your mold designs. ↩
-
Learn how improved wear resistance can extend the lifespan of your molds, saving costs and enhancing productivity. ↩