
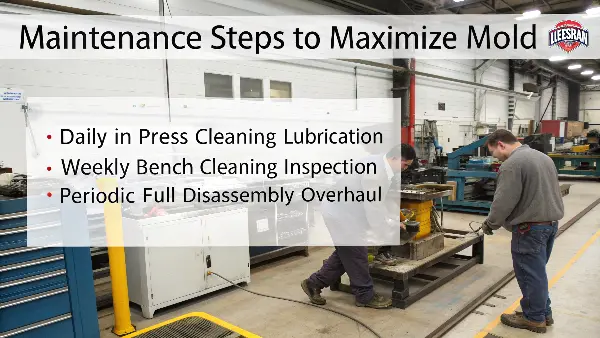
Molds wearing out prematurely causes costly downtime and quality issues. Don’t let preventable failures derail production. Proactive maintenance saves money and ensures consistent parts over the long haul.
Extend mold life through regular cleaning, proper lubrication of moving parts, detailed inspections for wear or damage, careful handling and storage, and addressing minor issues promptly before they become major failures requiring expensive repairs.
Waterline and Cooling Care
Cooling channels influence cycle time and dimensional stability. Scale, corrosion or blockage can create hot spots and longer cycles. Waterline maintenance is especially important for repeat production and multi-cavity molds where small temperature differences can become cavity variation.
Wear Points to Watch
Guide pins, bushings, ejector pins, return pins, slides, lifters, parting line shutoffs and support surfaces should be checked regularly. Wear often starts small, then becomes flash, sticking or broken components.
Use the Mold-Base Condition as the Maintenance Baseline
Record plate and support condition, guidance and locating wear, corrosion, circuit condition and alignment before setting the maintenance plan. Compare observations with the tool’s approved drawings and component limits.
Tool-life and construction classes belong in the mold-life specification review. A class label or nominal shot count does not determine the inspection interval or prove that a particular base remains serviceable.
What Really Causes Your Injection Molds to Wear Out?
Molds don’t last forever, even Class 101 tools, but premature failure is often preventable and generally frustrating. Simply running parts isn’t the only stress; many factors combine to cause wear and tear. Identifying these helps you target your maintenance efforts effectively.
Mold life is primarily reduced by abrasive/corrosive plastic resins, high injection pressures/temperatures, fast cycle times, inadequate cooling, improper handling/storage, incorrect machine setup (e.g., clamp force), lack of cleaning/lubrication, and delayed repairs of minor damage.
Every injection cycle contributes tiny amounts of wear. Over thousands or millions of cycles, this adds up. Several factors accelerate this process:
- Plastic Material: This is huge. Resins containing abrasive fillers like glass fibers or minerals act like sandpaper, eroding gates, runners, and cavity surfaces. Corrosive resins like PVC can chemically attack mold steels, especially non-stainless grades. Understanding the resin is step one.
- Processing Parameters: Running the mold aggressively takes a toll. High injection pressures and speeds increase erosion, especially at gate areas. High melt temperatures increase thermal stress on the steel. Very fast cycle times mean more frequent mechanical action and can lead to thermal fatigue if cooling isn’t optimal.
- Mold Design: Sometimes the design itself contributes to wear. Poor venting can cause gas traps and burning, damaging the steel surface. Inadequate cooling can lead to uneven temperatures, causing stress and potentially warpage of mold components over time. Sharp internal corners can be stress concentrators.
- Machine Setup: Excessive clamp force is a setup risk. It doesn’t necessarily prevent flash but can crush vents, hob the parting line (coining), and damage mold components. Misaligned machine platens put uneven stress on the mold.
- Handling and Storage: Physical damage from dropping, hitting, or improper prying during setup or removal shortens life. Storing a mold without proper cleaning and rust preventative, especially in humid environments, leads to corrosion that damages critical surfaces.
Lack of Maintenance: This is the most controllable factor. Resin residue buildup impairs cooling and venting. Lack of lubrication causes friction, galling, and seizure of moving parts like ejector pins, slides, and lifters. Small chips or damage left unaddressed can propagate into larger failures.
| Factor | How it Causes Wear/Damage | Mitigation Example |
|---|---|---|
| Abrasive Resin | Erosion of steel surfaces, gates | Use hardened tool steel inserts (H13+) |
| Corrosive Resin | Chemical attack, rust | Use stainless mold steel (S136) |
| High Pressure/Speed | Erosion, steel fatigue | Optimize process, use wear-resistant steel |
| Poor Venting | Burns, gas traps, surface damage | Regular vent cleaning, proper design |
| Excess Clamp Force | Crushed vents, parting line damage (coining) | Use calculated clamp force, proper setup |
| Lack of Lubrication | Friction, galling, seizure of moving parts | Regular lubrication schedule |
| Improper Storage | Rust, corrosion, physical damage | Clean, apply rust preventative, store safely |
Understanding these factors helps you anticipate potential problems and focus maintenance where it’s needed most. For the project team’s projects, considering the resin type and expected volume helps anticipate wear patterns from the design stage.
Plan Access, Inspection and Corrective Work for the Base
Define how technicians will inspect guide components, support surfaces, locating features, water connections and corrosion-prone areas safely under the site’s isolation procedure. Record measured wear, leaks, alignment findings and replaced components against the mold ID.
Choose inspection and service intervals from the tool’s operating duty, component instructions and condition history. Use the preventive-maintenance schedule guide for the wider maintenance program rather than treating a generic daily or shot-count interval as a requirement for every mold.
What Problems Signal Your Mold Needs Attention or is Wearing Out?
Seeing defects in your molded parts is often the first obvious sign that something is wrong with the mold. Ignoring issues like flash, burn marks, or sticking parts might seem minor initially, but these are frequently symptoms of underlying mold wear or maintenance needs. Recognizing these signs early prevents bigger failures and costly downtime.
Common part defects signaling mold wear or maintenance needs include flash (worn parting line, damaged vents), short shots (blocked vents, worn gates), burn marks (clogged vents), sticking parts (worn/galled ejectors, damaged surface), and dimensional inconsistency (worn locating features, cooling issues).
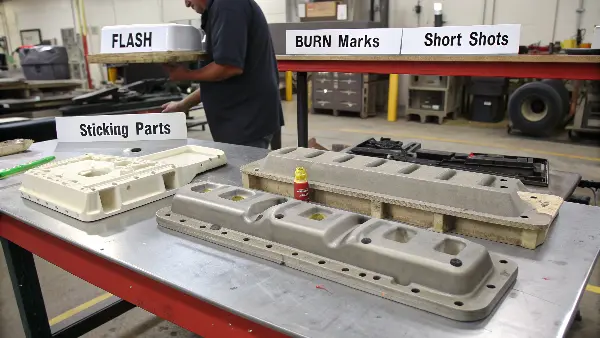
Your molded parts act as a diagnostic tool for the mold’s health. When you see consistent defects, investigate the mold:
- Flash: Plastic squeezing out at the parting line, around ejector pins, or slide actions.
- Potential Mold Causes: Worn or damaged parting line surfaces, crushed or blocked vents allowing pressure buildup, worn ejector pin holes, excessive clearance in slide components, bent plates due to improper support. Needs inspection and potentially repair/refurbishment. Lack of cleaning can also contribute.
- Short Shots / Non-Fills: The cavity doesn’t fill completely.
- Potential Mold Causes: Blocked vents preventing air escape (needs cleaning!), clogged, damaged or dimensionally changed gates affecting flow, leaking check ring on the machine (less likely a direct mold wear issue, but affects the process).
- Burn Marks: Black or brown streaks/spots on the part, often at the end of fill.
- Potential Mold Causes: Clogged or inadequate vents trapping and compressing air, which heats up and burns the plastic. Vents need cleaning or potentially need to be added/enlarged.
- Sticking, Drag Marks, Ejector Pin Marks: Parts are difficult to eject or show signs of damage during ejection.
- Potential Mold Causes: Roughness or damage on cavity/core surfaces (needs polishing/repair), worn or insufficient draft angles, galled or mushroomed ejector pins (need lubrication/replacement), worn ejector sleeves.
- Warpage / Dimensional Instability: Parts are distorted or dimensions vary significantly.
- Potential Mold Causes: Inconsistent or ineffective cooling due to clogged water lines (needs flushing/cleaning), significant wear on locating features (interlocks, leader pins) allowing misalignment.
- Surface Imperfections: Scratches, dents, or other marks transferred from the mold surface.
Potential Mold Causes: Physical damage to the cavity/core surfaces from handling, improper cleaning tools, or debris. Needs careful polishing or repair.
| Defect | Potential Mold-Related Cause | Maintenance Link |
|---|---|---|
| Flash | Worn/Damaged PL, Blocked Vents, Worn Pins/Slides | Inspection, Cleaning, Repair, Component Replace |
| Short Shot | Blocked Vents, Worn Gates | Vent Cleaning, Gate Inspection/Repair |
| Burns | Clogged/Inadequate Vents | Vent Cleaning, Potential Design Mod |
| Sticking | Rough Surface, Worn/Galled Ejectors, No Draft | Polishing, Lubrication, Ejector Replace |
| Warpage | Clogged Cooling, Worn Locators | Cooling Channel Cleaning, Locator Inspect/Replace |
| Scratches | Damaged Cavity/Core Surface | Careful Handling, Polishing/Repair |
Treating these defects purely as processing issues without checking the mold is a mistake. Often, the root cause lies in the tool itself, signaling that maintenance or repair is overdue. Early detection and correction save time and money.
Mold base maintenance is one of the quiet ways to protect tooling investment. A mold may be designed well and built accurately, but poor maintenance can lead to rust, wear, waterline blockage, ejection problems, flash, dimensional drift and unexpected downtime.
Maintenance Should Be Scheduled
Waiting until defects appear is not maintenance. A practical schedule should include cleaning, lubrication, vent checks, waterline inspection, ejector review, slide/lifter inspection, rust prevention and storage control. The frequency depends on resin, volume, cycle conditions and tool complexity.
Maintenance Records Matter
Good records show what was cleaned, repaired, replaced and observed. For export molds or repeat orders, these records help identify whether a problem is normal wear, misuse, material effect or design weakness.
Project-Specific Buyer Checklist
- Cleaning schedule defined
- Lubrication points documented
- Waterlines inspected
- Wear parts checked
- Maintenance history recorded
How CKMOLD Would Review the Project
For next steps, contact CKMOLD with your drawings and expected quantity. If the project needs production support, review production injection molding; for higher output, see multi-cavity mold manufacturing; for export tooling, see export injection mold manufacturing; and for mold life issues, see mold repair and modification.
FAQ
Why is mold base maintenance important?
It protects alignment, cooling, ejection, mold life and production stability.
How often should a mold be maintained?
Frequency depends on resin, volume, cycle conditions and tool complexity.
Can poor waterlines affect part quality?
Yes. Blocked or scaled waterlines can cause hot spots, warpage and cycle delays.
What parts wear most often?
Guide components, ejector pins, slides, lifters and shutoff areas are common wear points.
Can CKMOLD support mold maintenance review?
Yes. CKMOLD can review mold condition, repair needs and maintenance planning.
Conclusion
Proactive, scheduled mold maintenance isn’t an expense; it’s an investment. Tailoring the plan to the mold class and operating conditions prevents costly downtime, ensures part quality, and extends the valuable life of your injection molds significantly beyond neglect.
Primary References for This Topic
- ISO: Quality Management Systems — An Introduction — The QMS principles of documented processes, records, monitoring and improvement support a traceable preventive-maintenance program.
- EUROMAP Technical Recommendations — Use the applicable machine–mold interface recommendations when checking clamps, centering, services and mold-transfer compatibility.
- HASCO: Precision for Mouldmaking — A primary component-maker overview of standardized mold-base systems; maintenance limits still belong to the actual component and mold records.
Separate a Mold Fault From a Process Drift
Record defect location by cavity, when it began, recent material or setting changes, coolant flow/temperature and the last accepted sample. Compare repeatable symptoms with the approved process window before attributing every defect to wear. Isolate and inspect the tool under the site procedure; do not increase clamp force or grind a vent simply to hide a symptom.
For a repair enquiry, provide the mold ID, assembly drawing, cycle/maintenance history, defect photos and measured wear. Agree the repair acceptance test, spare components and the first-run inspection. This article concerns base condition; the mold-life planning guide covers service commitments and replacement economics.