Material
Recyclable Plastic Container Solutions: How to Design for End-of-Life?
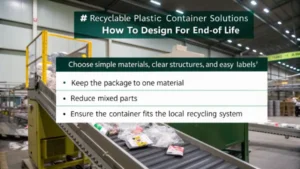
Design recyclable plastic containers by checking resin, labels, pigments, local collection routes and reuse conditions before mold release.

Design recyclable plastic containers by checking resin, labels, pigments, local collection routes and reuse conditions before mold release.
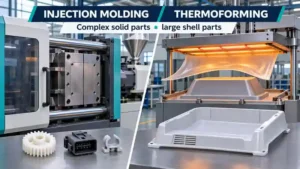
Choose between injection molding and thermoforming from the part geometry, critical dimensions, material form and cost per accepted part at the expected volumes. Injection molding fills a closed tool and can integrate detailed features on both sides. Thermoforming shapes heated sheet and is often a strong candidate for large open
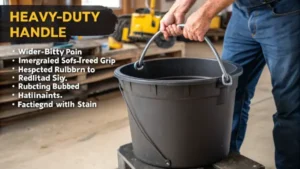
Integrated handles can improve bucket-carrying comfort when grip size, attachment geometry and materials suit the filled load, intended users and task. A wider contact area can distribute pressure across the palm, but handle design alone cannot eliminate pain or make an excessive load acceptable. Start with a grip that fits
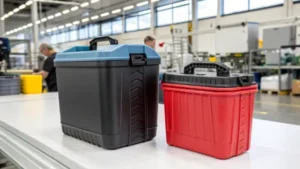
Two-component molding is worth considering when an integrated grip, seal or color feature removes a separate assembly step or provides a function that a single material cannot meet. The decision depends on the exact material grades, bond or retention design, tooling, production demand and acceptance tests. Appearance alone does not
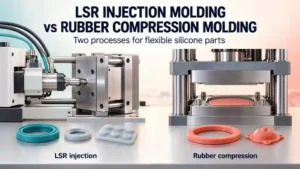
There is more than one way that silicone can be used for seals, gaskets, keypads, valves, and soft-touch parts. There are two predominant methods, namely liquid silicone rubber (LSR) injection molding and rubber compression molding. They both generate flexible, durable elastomer components but vary in material, tooling, speed, precision, and
Ribs can increase a bucket wall’s bending stiffness without thickening the entire wall. Whether they allow a lighter bucket depends on the resin grade, load direction, geometry and service conditions. A design must still meet its filled-bucket drop, handle-load and sustained stacking requirements; adding ribs alone does not prove that
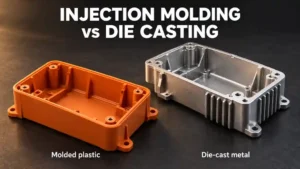
Choose injection molding when a specified polymer can meet the part’s loads, temperature, chemical exposure and dimensional requirements at an acceptable total cost. Consider die casting when the design needs a metal alloy’s stiffness, heat conduction or other properties. Validate the complete part and assembly: neither process name establishes performance
Reduce a plastic container’s weight by removing unnecessary material or selecting a lower-density structure while meeting its specified function. Compare geometry, material and process changes against the actual contents, load, temperature, stacking duration, drop conditions, closure and barrier requirements. Lower mass, lower resin consumption and lower cost are different outcomes;
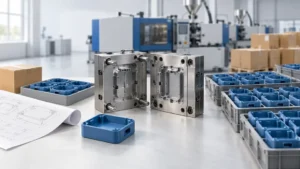
You have a molded component you’re ready to make, and your supplier asks a simple question: Is this a one-off or a continuing supply? The solution determines your pricing, the capacity that the supplier offers you, who has the inventory in place, and what happens to the mold when your
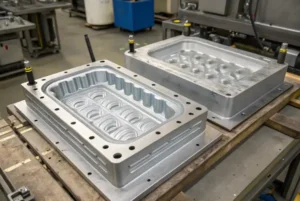
For a large plastic container mold, use cooling zones that match the local heat load and the plant’s available coolant flow and pressure. Start with accessible drilled circuits, then evaluate baffles, bubblers, conductive inserts or conformal inserts for areas that remain difficult to cool. Channel size, spacing and distance from
Optimize a bucket mold by reducing cost per accepted bucket while maintaining its specified drop, stacking/creep, handle-load, lid-fit and dimensional performance. First measure the cycle bottleneck, part and scrap mass, reject rate and actual cooling conditions. Then compare geometry, gate/runner, cooling and process changes on the same acceptance basis; thinner
Tamper evidence and child resistance address different risks. A breakaway band or liner can indicate first opening; it does not make a bucket child-resistant. A child-resistant closure must be assessed as a complete package under the applicable product and market requirements, including adult usability and reclosure where relevant. Design Tamper
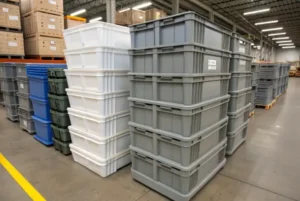
Stackable container design can improve space use by matching footprints, stack interfaces and usable internal volume to the pallet or rack. Safe height is limited by the container, load, temperature, handling equipment and facility clearance requirements. A matching lid and base alone do not establish a safe floor-to-ceiling stack. What
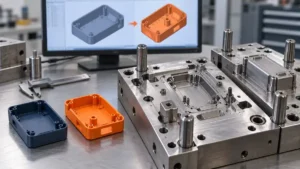
If your product design changes after tooling starts, first confirm which engineering, purchasing and machining operations are complete, pause the affected work and issue the current and proposed drawing revisions. The mold maker must assess whether the change can be machined, welded or handled with replacement inserts, then quote the
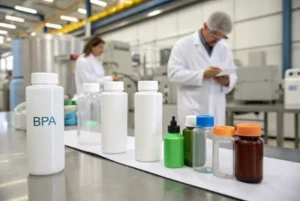
BPA-free describes a specific substance claim, not the safety of the complete container. PP, PET, HDPE and selected copolyester grades can be candidates, but the exact resin, additives, colorants, closure and intended use must be assessed together. Start with food type, contact time, temperature, cleaning method and destination market before
“Next-generation TPE” is not a standardized material class. It is a useful market description for thermoplastic-elastomer grades developed for a particular improvement—such as recycled or bio-based content, adhesion to a selected substrate, lower density, softness, weathering or a demanding mechanical property. No grade improves every property at once. Select the
Selected TPE and TPV grades can be useful for automotive seals when their weathering, fluid resistance and compression behavior match the application. TPE is a broad material category. Specify the actual fluid, temperature, deflection, service duration and qualification tests before comparing it with EPDM or another elastomer. A seal should
Before paying a tooling charge, document which mold and components the charge covers, the intended ownership and title-transfer event, and the rights to custody, maintenance, files and release. Payment wording alone may leave these questions unresolved. Have the transaction documents reviewed under the applicable law rather than assuming that one
USP Plastic Class VI and ISO 10993 are not two levels of the same approval. USP <88> describes defined in-vivo biological-reactivity tests for plastics and assigns test classifications under specified extraction and exposure conditions. ISO 10993-1:2025 is a risk-management framework for planning the biological evaluation of a medical device according
Selecting a TPE for a medical-device component is a device risk-management task, not a search for a generic “medical-grade” plastic. Start with the component’s body-contact category, duration, function, cleaning or sterilization exposure and regulatory pathway. Then select and validate an exact supplier grade. What makes a TPE candidate suitable for