
A shrinkage-rate database is useful, but it is not a substitute for engineering judgment. The number you find online or in a material sheet only becomes reliable when it is connected to resin grade, test method, wall thickness, flow direction and the actual mold/process plan.
Start with the selected resin manufacturer’s current grade document. For a structured entry point, BASF’s materials and documents resources provides product finders, document access and a route to CAMPUS. Search by the complete grade designation, then check the manufacturer, document revision and test conditions. If directional shrinkage or a required condition is missing, request it from the supplier rather than substituting an unlabeled family range.
For the complete pre-tooling framework, use Injection Molding Shrinkage Risk Review Before Tooling. This page stays focused on selection and interpretation of grade-specific data.
What Exactly Is the Shrinkage Rate in Injection Molding?
Linear molding shrinkage compares a molded dimension with the corresponding mold-cavity dimension under defined molding and measurement conditions. When referenced to the mold dimension, S = (Lm − Lp) / Lm. It is not simply the thermal contraction of an unconstrained melt to room temperature. Record measurement timing, conditioning, direction and units before using the value.
- Material Type: Amorphous plastics (like ABS, PC) generally shrink less and more uniformly than semi-crystalline plastics (like PP, Nylon).
- Additives: Fillers like glass fibers or talc typically reduce shrinkage but can make it directional.
-
Processing Conditions: Mold temperature, melt temperature, packing pressure, and cooling time all play significant roles.
Select a Traceable Grade Value Instead of a Family Average
A material-family range does not identify a tool-design allowance. Obtain the exact grade document and record test method, specimen thickness, molding conditions, measurement timing and flow direction. For reinforced grades, keep flow and transverse values separate.
Confirm the HIPS Grade and Measurement Conditions
Use the selected HIPS supplier’s current data rather than a fixed percentage for every HIPS part. Check whether the specimen, wall, packing and conditioning conditions are relevant to the feature being sized, and record uncertainty for the trial plan.
So, How Do You Actually Calculate Shrinkage for an Injection Mold?
To calculate the mold dimension, use the formula: Mold Dimension (Lm) = Part Dimension (Lp) / (1 – Shrinkage Rate (S)). ‘S’ must be the decimal form of the material’s specific shrinkage percentage.
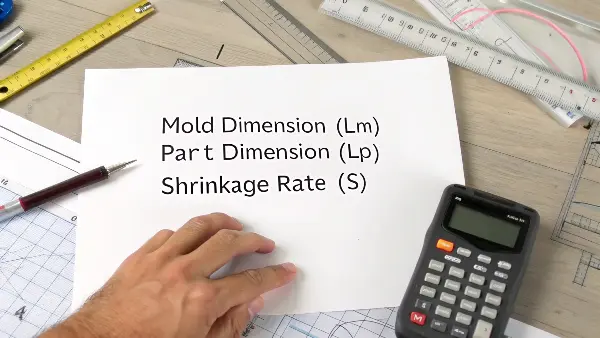
Illustrative reference image; it does not establish a tested material, measured tolerance or verified CKMOLD customer result.
Lm = Lp / (1 - S)
Let’s break this down:
Lmis the Mold Dimension. This is the actual size you need to make the corresponding feature in the mold cavity.Lpis the desired Part Dimension. This is the final size you want that feature to be on the cooled plastic part, as per your design specification.-
Sis the Shrinkage Rate of the specific plastic material you’re using, expressed as a decimal. So, if a material datasheet says the shrinkage is 1.5%, you useS = 0.015.Illustrative arithmetic only: if a 150 mm feature uses an assumed linear shrinkage of 0.5% referenced to the mold dimension, then S = 0.005 and:
Lm = 150mm / (1 - 0.005) = 150mm / 0.995 = 150.7537... mmThe calculated value is approximately 150.75 mm. This arithmetic example does not select the production shrinkage allowance; validate the grade, direction, measurement state and steel-safe approach before cutting the feature.
Use the exact grade’s supplier data as a documented starting assumption. Where flow and transverse values differ, retain both and review their relevance to the actual orientation and geometry. Applying two independent scale factors does not by itself predict or prevent warpage; constrained geometry, packing and cooling need separate review.
Why Shrinkage Databases Disagree
Different databases may show different values because they use different specimens, wall thicknesses, processing temperatures and measurement methods. Some values are broad family ranges, while others are grade-specific. A buyer should ask whether the value is good enough for early estimating or precise enough for tool steel sizing.
How to Read Material Supplier Data
For engineering plastics, check whether the sheet separates flow direction from transverse direction and whether the value applies to a specific test plaque. Filled resins often shrink less in the flow direction but may create more directional warpage. That distinction is critical for housings, connectors and precision assemblies.
When Database Values Need Adjustment
The value may need adjustment for thick walls, uneven ribs, high packing pressure, gate location, mold temperature or post-mold conditioning. Hygroscopic materials such as nylon also require attention because moisture conditioning can change final dimensions after molding.
Turn Grade Data Into a Tooling Assumption
Use supplier data, geometry review and relevant controlled trial records, when available, to propose the initial tool allowance. Record where a previous part or process differs. Identify dimensions needing steel-safe stock or replaceable inserts, and define the measurements and authority needed to release a correction after trial.
Buyer and Engineering Checklist
- Prioritize grade-specific supplier data over generic material-family tables.
- Check whether the database separates flow and cross-flow shrinkage.
- Record wall thickness and test conditions when quoting a shrinkage number.
- Use historical trial data for similar parts when available.
- Treat database values as assumptions that must be validated during sampling.
FAQ
Where should buyers get shrinkage-rate data?
Start with the resin supplier data sheet, then compare reputable material databases and previous project history. For precision tooling, final decisions should be confirmed through trial measurement.
Why is a single shrinkage number risky?
Because actual shrinkage changes with grade, filler, flow direction, wall thickness and process settings. A single number can hide the variation that causes dimensional problems.
Build a Traceable Grade-Specific Shrinkage Record
Record manufacturer, exact grade and color, document revision, test method, specimen thickness, flow/cross-flow values and molding conditions. Keep linear and volumetric data in separate fields; a family label cannot define a guaranteed shrinkage bound.
If two sources disagree, first check whether they describe the same grade and test. Do not average incompatible values. Request the resin supplier’s current document and retain the original file alongside the tool-design assumption. ASTM D955 warns that standard specimens do not predict absolute shrinkage in every production geometry.
A useful RFQ states which grade is fixed and which substitutions remain open. Send that record with the CTQ drawing through the enquiry form; ask the moldmaker to explain how uncertainty will be handled at trial.
Technical reference: ASTM D955-21 public scope and limitations. The calculation and scale-factor guide addresses the related decision separately.
Conclusion
Keep the grade document, test conditions and chosen tooling assumption together. Resolve missing or conflicting data before releasing critical steel dimensions, and update the assumption from controlled trial measurements. The calculation remains a traceable estimate until the actual part, tool and process have been validated.