
Choosing between molding pressures feels complex? This decision impacts component integrity, cost, and production speed. Let’s simplify it.
Conventional thermoplastic injection molding and low-pressure hot-melt encapsulation differ in materials, equipment, pressure and end-use requirements. Compare grade- and machine-specific windows; bar is a pressure unit, not force, and neither process has a universal temperature/pressure range.
Understanding the nuances between high-pressure and low-pressure injection molding is crucial for any product designer or engineer like Jacky. For years, I’ve seen projects succeed or stumble based on this fundamental choice. At CKMOLD, we believe in empowering you with knowledge. This guide will walk you through the key differences, helping you select the best approach for your specific application, ensuring both quality and efficiency. Let’s dive in.
What is the Core Difference Between Low Pressure and High Pressure Molding?
Confused about how low and high pressure molding truly differ? This uncertainty can lead to selecting a suboptimal process, affecting part quality.
The primary difference lies in the applied pressure and temperature. High pressure uses significantly greater force and heat, suitable for intricate, robust parts. Low pressure employs much gentler conditions, making it ideal for encapsulating delicate electronic components.
When we talk about injection molding, the "pressure" aspect is fundamental. It dictates how the molten plastic fills the mold cavity and the characteristics of the final part. I’ve worked on countless projects where understanding this distinction was key. High-pressure molding is the traditional workhorse for many plastic parts, while low-pressure molding has carved out a vital niche, especially with the rise of integrated electronics.
Key Distinguishing Factors
| Let’s break down the main areas where these two processes diverge: | Feature | Low-Pressure Molding (LPM) | High-Pressure Molding (HPM) |
|---|---|---|---|
| Pressure Basis | Material/system-specific; identify the measurement location | Machine/material/geometry-specific; distinguish hydraulic, melt and cavity pressure | |
| Temperature | Follow the hot-melt grade and component-exposure limit | Follow the thermoplastic grade and mold requirements | |
| Mold Material | Often Aluminum | Typically Steel (P20, H13, etc.) | |
| Cycle Time | Depends on geometry, cooling and handling | Depends on geometry, cooling and handling | |
| Tooling Cost | Quote actual interfaces, cavities and support | Quote actual interfaces, cavities and support | |
| Part Stress | Verify insert exposure and final stress/adhesion | Verify process stress and part/insert function | |
| Primary Use | Encapsulation, overmolding fragile components | Complex parts, high volume, structural items |
Thinking about it from a practical standpoint, if you, like Jacky, are designing a rugged enclosure for a consumer electronic device, HPM is likely your go-to. But if you need to encapsulate a delicate sensor array directly on a PCB, LPM offers the gentle touch required.
How Does Pressure Affect Injection Molding Overall?
Unsure how varying pressure impacts your molded parts? Incorrect pressure leads to defects like short shots, flash, or weak spots.
Pressure in injection molding dictates melt flow into the cavity, part density, surface finish, and dimensional accuracy. Proper pressure ensures complete filling, good replication of mold details, and minimizes internal stresses for a quality part.
Pressure is one of the most critical parameters in the entire injection molding process. It’s not just about pushing plastic into a hole; it’s a carefully controlled force that shapes the outcome. I always tell my clients at CKMOLD that getting the pressure profile right – from initial fill to pack and hold – is an art and a science.
The Critical Roles of Pressure
Let’s explore what pressure actually does:
- Driving Material Flow: The primary role of injection pressure is to push the molten plastic from the machine’s nozzle, through the runner system and gate, and into the mold cavity. It needs to overcome the flow resistance, which depends on material viscosity, mold geometry, and temperature. Too little pressure, and you get a "short shot" – an incomplete part. I’ve seen this happen when a machine isn’t quite powerful enough for the mold or the material is too viscous.
- Ensuring Part Compaction (Packing): Once the cavity is mostly full, "packing pressure" (or holding pressure) is applied. This phase is crucial for several reasons:
- It compensates for material shrinkage as the plastic cools.
- It forces the plastic to conform tightly to the mold surface, accurately replicating textures and fine details. Jacky would appreciate this for aesthetic parts.
- It helps achieve the desired part density and mechanical properties.
- Managing Defects:
- Too High Pressure: Can lead to "flash" (excess material squeezing out of the mold parting line), excessive stress in the part (leading to warpage or cracking), and even damage to the mold or machine.
- Too Low Pressure: Results in short shots, sink marks (depressions on the surface), voids (internal bubbles), and poor surface finish.
The skill of a good molding technician lies in finding that "sweet spot" for pressure settings, often involving a multi-stage profile.What Exactly is High-Pressure Injection Molding?
Curious about the specifics of high-pressure molding? Not knowing its capabilities can mean missing out on its benefits for complex parts.
High-pressure injection molding (HPM) is a conventional process using the pressure and temperature required by the material, flow resistance and validated machine setup to melt, inject, and form plastic into precise shapes. It’s favored for high-volume production and intricate component designs.
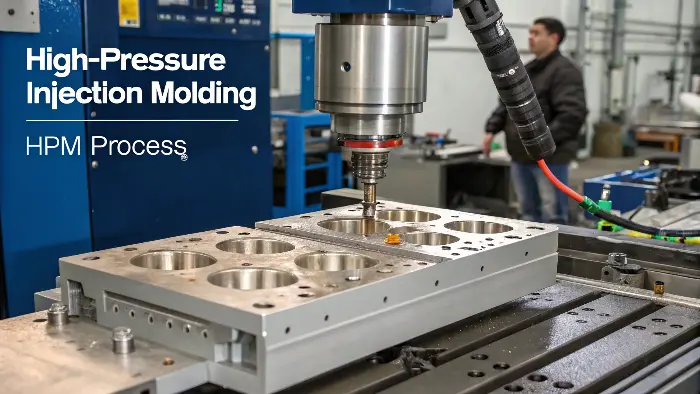
High-pressure injection molding is what most people picture when they think of "injection molding." It’s the workhorse of the plastics industry, responsible for producing an enormous variety_of parts we use every day, from car dashboards to toy components. At CKMOLD, we’ve designed and managed production for countless HPM projects.
Diving Deeper into HPM
This method has been refined over decades and offers several advantages:
- Capability for Complex Geometries: The high pressures ensure that molten plastic can be forced into very intricate mold cavities, filling thin walls, sharp corners, and detailed features. This is critical for designers like Jacky who are often pushing the boundaries of part complexity for consumer electronics. For example, creating snap-fits, living hinges, or complex rib patterns is well within HPM’s capabilities.
- Wide Material Compatibility: HPM can process a vast range of thermoplastic materials, from common commodity plastics like polypropylene (PP) and polyethylene (PE) to engineering-grade resins like polycarbonate (PC), ABS, nylon (PA), and even high-performance polymers like PEEK. This versatility makes it suitable for a broad spectrum of applications.
- High Production Efficiency: HPM machines are typically designed for fast cycle times. Combined with multi-cavity molds, this allows for very high output rates, making it economical for mass production. I’ve seen machines churning out thousands of parts per hour.
- Good Mechanical Properties: The high packing pressures help to create dense parts with good mechanical strength and dimensional stability, provided the process is well-controlled.
However, HPM also requires tooling designed for the actual loads, material and production duty to withstand the high clamping forces and injection pressures. This means tooling can be more expensive and take longer to produce compared to molds for low-pressure processes.
if you need more infor about fast cycle time and mold optimization please check out this article How Can You Optimize Your Mold’s Cooling System for Faster Cycles and Better Parts?
What are the Typical Pressures for Low-Pressure Injection Molding?
Wondering about the pressure range in low-pressure molding? Understanding this helps determine its suitability for protecting sensitive electronic components.
Low-pressure injection molding (LPM) uses a low-viscosity material and a supplier-defined process window at comparatively low injection pressure. This gentle process is key for overmolding delicate items without damage.
Low-pressure molding, sometimes called "gentle molding," is a fascinating and increasingly important technology. When I first encountered it, I was amazed at its ability to protect highly sensitive electronic components. The core idea is simple: use just enough pressure to encapsulate or overmold a part without causing any harm.
Understanding LPM Parameters and Benefits
The much lower pressures and often lower melt temperatures are what set LPM apart:
- Protecting Delicate Inserts: The primary advantage of LPM is its ability to overmold fragile components like printed circuit boards (PCBs), sensors, connectors, coils, and even glass elements. Some components cannot withstand the required pressure, temperature or handling; others can be conventionally insert-molded with suitable support and validation. Jacky, if you’re designing a product with embedded electronics that need environmental protection, LPM is a strong contender. I’ve seen it used to create watertight seals around USB connectors on a PCB, an application requiring validation of adhesion, leak resistance, component exposure and strain relief in the selected process.
- Reduced Tooling Costs: Because the clamping and injection forces are so much lower, molds for LPM can often be made from softer, less expensive materials like aluminum instead of hardened steel. This can lead to faster tool manufacturing times and lower upfront tooling investment.
- Specialized Materials: LPM typically uses specific thermoplastic materials, including qualified polyamide- or polyolefin-based hot melts; Henkel describes the material/process scope. This does not imply that every TPE is a low-pressure encapsulation resin. These materials are chosen for their low viscosity at processing temperatures, excellent adhesion to various substrates, and good sealing properties. They provide environmental protection against moisture, dust, vibration, and thermal shock.
- Applications: Common applications include:
- PCB Encapsulation: Protecting assembled circuit boards.
- Connector Overmolding: Creating robust and sealed cable assemblies.
- Sensor Protection: Encasing sensors for use in harsh environments.
- Strain Relief: Providing flexible strain relief for wires and cables.
The cycle times for LPM can sometimes be longer than HPM, depending on the material and part complexity, but the ability to integrate electronics directly into a molded assembly offers significant advantages in product design and functionality.
Give the Encapsulation Supplier a Component Exposure Limit
Specify the electronics/subassembly revision, keep-out areas, permitted pressure and temperature exposure, sealing target, wire strain relief, adhesion substrates and service environment. Check whether cooling, demolding, repairability and any post-process testing are acceptable for the assembly.
Ask for evidence on the actual encapsulant and component combination after thermal/humidity exposure, not just a generic low-pressure demonstration. Low injection pressure does not establish low thermal exposure, electrical compatibility or a watertight product.
Use the pressure root-cause guide for an existing molding defect. For a process-selection enquiry, provide the assembly drawing and acceptance tests so conventional molding, low-pressure hot melt and other protection routes can be compared on the same basis.
Conclusion
High-pressure excels for complex, high-volume parts; low-pressure gently protects delicate electronics. Choosing correctly hinges on your part’s specific needs, materials, and production volume.