
Struggling to find reliable shrinkage rates for different plastics? This uncertainty leads to design errors, costly mold rework, and project delays for product designers. You need accurate data.
A shrinkage-rate database is useful, but it is not a substitute for engineering judgment. The number you find online or in a material sheet only becomes reliable when it is connected to resin grade, test method, wall thickness, flow direction and the actual mold/process plan.
A comprehensive “database” is best compiled from material supplier datasheets, industry handbooks, and specialized software, as shrinkage varies greatly with material grade, additives, and processing conditions. This guide helps you navigate these sources.
Finding the exactshrinkage rate for every plastic imaginable in one single, universally accepted database can be a bit of a holy grail. I’ve spent years in this industry, and what I tell everyone, from budding designers to seasoned engineers like the designer, is that precision comes from diligence. You need to know where to look and how to interpret the data. The good news is, the information is out there, and understanding how to access and apply it will set you apart.
For the complete pre-tooling framework, use Injection Molding Shrinkage Risk Review Before Tooling. This page stays focused on selection and interpretation of grade-specific data.
What Exactly Is the Shrinkage Rate in Injection Molding?
Heard the term “shrinkage rate” but unsure what it truly means for your parts? Misunderstanding this fundamental concept often leads to dimensional inaccuracies and parts that don’t fit, causing major headaches.
The shrinkage rate is the percentage by which a plastic material contracts as it cools from its processing temperature in the mold to room temperature. This value is crucial for sizing mold cavities accurately.
- Material Type: Amorphous plastics (like ABS, PC) generally shrink less and more uniformly than semi-crystalline plastics (like PP, Nylon).
- Additives: Fillers like glass fibers or talc typically reduce shrinkage but can make it directional.
-
Processing Conditions: Mold temperature, melt temperature, packing pressure, and cooling time all play significant roles.
Understanding these nuances is key For the project team and anyone designing for injection molding.
Select a Traceable Grade Value Instead of a Family Average
A material-family range does not identify a tool-design allowance. Obtain the exact grade document and record test method, specimen thickness, molding conditions, measurement timing and flow direction. For reinforced grades, keep flow and transverse values separate.
Confirm the HIPS Grade and Measurement Conditions
Use the selected HIPS supplier’s current data rather than a fixed percentage for every HIPS part. Check whether the specimen, wall, packing and conditioning conditions are relevant to the feature being sized, and record uncertainty for the trial plan.

-
So, How Do You Actually Calculate Shrinkage for an Injection Mold?
You have the shrinkage rate, but how do you use it to design the mold cavity? Simply guessing or making the mold “a bit bigger” is not a professional approach and will likely fail for precise parts.
To calculate the mold dimension, use the formula: Mold Dimension (Lm) = Part Dimension (Lp) / (1 – Shrinkage Rate (S)). ‘S’ must be the decimal form of the material’s specific shrinkage percentage.
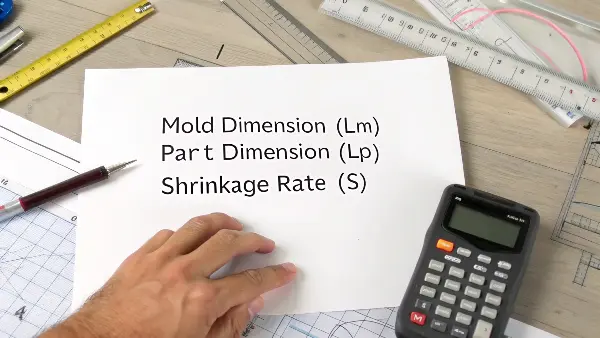
Okay, so we’ve talked about finding shrinkage rates. Now, let’s get practical with how the designer or any designer actually uses this information to size a mold cavity. The fundamental formula I use daily, and the one you should burn into your memory, is:
Lm = Lp / (1 - S)
Let’s break this down:
Lmis the Mold Dimension. This is the actual size you need to make the corresponding feature in the mold cavity.Lpis the desired Part Dimension. This is the final size you want that feature to be on the cooled plastic part, as per your design specification.-
Sis the Shrinkage Rate of the specific plastic material you’re using, expressed as a decimal. So, if a material datasheet says the shrinkage is 1.5%, you useS = 0.015.Illustrative arithmetic only: if a 150 mm feature uses an assumed linear shrinkage of 0.5% referenced to the mold dimension, then S = 0.005 and:
Lm = 150mm / (1 - 0.005) = 150mm / 0.995 = 150.7537... mmThe calculated value is approximately 150.75 mm. This arithmetic example does not select the production shrinkage allowance; validate the grade, direction, measurement state and steel-safe approach before cutting the feature.
It’s crucial to get
Sfrom the material supplier’s datasheet for the exact gradeof plastic. General values are starting points, but specific grades, especially those with fillers (like glass fibers), can behave differently. For glass-filled materials, you’ll often see two shrinkage values: one for “flow direction” and one for “cross-flow direction.” This is because the fibers align with the flow, restricting shrinkage in that direction more than across it. In such cases, you have to apply these different rates to your mold dimensions accordingly, which is critical for preventing warpage.Why Shrinkage Databases Disagree
Different databases may show different values because they use different specimens, wall thicknesses, processing temperatures and measurement methods. Some values are broad family ranges, while others are grade-specific. A buyer should ask whether the value is good enough for early estimating or precise enough for tool steel sizing.
How to Read Material Supplier Data
For engineering plastics, check whether the sheet separates flow direction from transverse direction and whether the value applies to a specific test plaque. Filled resins often shrink less in the flow direction but may create more directional warpage. That distinction is critical for housings, connectors and precision assemblies.
When Database Values Need Adjustment
The value may need adjustment for thick walls, uneven ribs, high packing pressure, gate location, mold temperature or post-mold conditioning. Hygroscopic materials such as nylon also require attention because moisture conditioning can change final dimensions after molding.
How CKMOLD Uses Data in Tooling Decisions
CKMOLD treats shrinkage data as an input to DFM, not as the final answer. The team combines supplier data, geometry review, previous molding experience and trial measurement to decide whether a dimension should be cut to nominal, biased steel-safe or protected for later adjustment.
Buyer and Engineering Checklist
- Prioritize grade-specific supplier data over generic material-family tables.
- Check whether the database separates flow and cross-flow shrinkage.
- Record wall thickness and test conditions when quoting a shrinkage number.
- Use historical trial data for similar parts when available.
- Treat database values as assumptions that must be validated during sampling.
FAQ
Where should buyers get shrinkage-rate data?
Start with the resin supplier data sheet, then compare reputable material databases and previous project history. For precision tooling, final decisions should be confirmed through trial measurement.
Why is a single shrinkage number risky?
Because actual shrinkage changes with grade, filler, flow direction, wall thickness and process settings. A single number can hide the variation that causes dimensional problems.
Build a Traceable Grade-Specific Shrinkage Record
Record manufacturer, exact grade and color, document revision, test method, specimen thickness, flow/cross-flow values and molding conditions. Keep linear and volumetric data in separate fields; a family label cannot define a guaranteed shrinkage bound.
If two sources disagree, first check whether they describe the same grade and test. Do not average incompatible values. Request the resin supplier’s current document and retain the original file alongside the tool-design assumption. ASTM D955 warns that standard specimens do not predict absolute shrinkage in every production geometry.
A useful RFQ states which grade is fixed and which substitutions remain open. Send that record with the CTQ drawing through the enquiry form; ask the moldmaker to explain how uncertainty will be handled at trial.
Technical reference: ASTM D955-21 public scope and limitations. The calculation and scale-factor guide addresses the related decision separately.
Conclusion
Finding precise shrinkage rates requires consulting supplier datasheets and understanding material families. Applying these correctly in calculations is key for accurate mold design and successful part production, benefiting product designers immensely.