
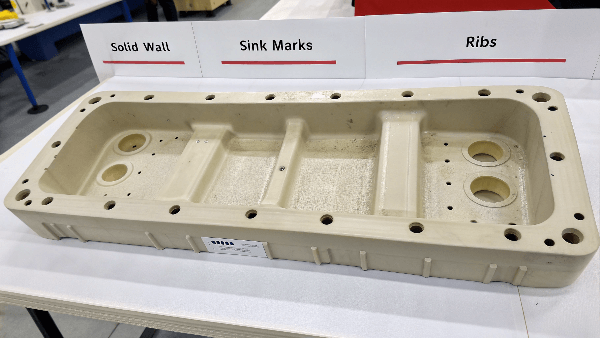
Thin-wall and thick-wall injection molding create very different engineering problems. Thin walls challenge filling speed, pressure, venting, and gate design. Thick walls challenge cooling time, sink marks, voids, shrinkage, and warpage. The right design is not thin or thick by default; it is the wall strategy that supports function, cost, moldability, and production stability.
Thin-Wall Molding Risks
Thin-wall parts reduce weight and cycle time, but they require enough flow capability to fill before the melt freezes. Long flow paths, sharp turns, poor venting, or small gates can create short shots and weak weld lines. Thin-wall projects often need careful material selection, higher injection speed, and a mold designed for fast filling.
Thick-Wall Molding Risks
Thick walls may look strong, but they can create sink marks, voids, long cooling time, internal stress, and warpage. A thick boss or rib base can drive the entire cycle time. When strength is needed, ribs, gussets, and better geometry often work better than simply adding material.
Material Selection
High-flow materials can help thin walls, while low-shrink or reinforced materials may help dimensional stability. But every material choice has trade-offs. Glass fiber can improve stiffness but create warpage and surface concerns. Soft materials may need different wall strategy than rigid engineering resins.
Mold Design and Cooling
Thin walls need balanced filling, venting, and suitable gates. Thick walls need cooling control and steel-safe planning for shrinkage. Both need DFM review before tooling. Cooling design is especially important because wall thickness controls how quickly heat leaves the part.
How Buyers Should Specify Requirements
A drawing should identify functional walls, cosmetic areas, tolerance-critical features, and structural requirements. If the design is still flexible, ask for DFM feedback before locking thickness. CKMOLD can review whether a wall strategy is realistic for the resin and production quantity.
RFQ and Validation Checklist
- 3D CAD file and 2D drawing with critical dimensions marked
- Material grade, color, surface finish, texture and performance requirements
- Expected annual volume, prototype quantity or production batch size
- Cosmetic, assembly, packaging and inspection requirements
- Current samples, defect photos or prior mold information if available
- Target market requirements such as UL, RoHS, REACH, UV exposure or other compliance needs when relevant
Engineer-to-Engineer Notes
A practical engineering review should separate confirmed facts, assumptions and open questions. Facts may include material grade, part weight, wall thickness, machine size and measured dimensions. Assumptions may include expected volume, acceptable cosmetic limits or whether a material substitute is allowed. Open questions may include compliance, assembly force, outdoor exposure, packaging or whether a visible surface can accept a gate mark.
Project Risk Review Before Tooling
Before a mold is approved for manufacturing, the buyer and supplier should identify the top three risks in the project. For one part, the main risk may be wall thickness and sink. For another, it may be resin drying, cosmetic surface quality, gate location, cavity balance, or a tolerance that is too tight for the material. Naming the risks early makes the trial plan more focused.
Sample Approval Should Follow the Real Use Case
Approval should also record what changed after each trial. If a gate was enlarged, cooling was changed, steel was adjusted, or process settings were narrowed, the customer should know. This record protects repeat orders because the next production run has a clear baseline instead of relying on memory.
Common Mistakes to Avoid
- Approving samples only by photos without dimensions or functional checks
- Comparing mold quotes without checking steel, cavity count, trial rounds and correction responsibility
- Choosing material by name without reviewing service conditions and molding behavior
- Ignoring packaging and handling until after the parts are already molded
- Changing product design after tooling starts without updating drawings and approval records
Supplier Evaluation Notes
How Purchasing and Engineering Teams Should Use This
FAQ
What is thin-wall injection molding?
It is molding parts with relatively thin sections that require careful flow, pressure, venting and cooling control.
Are thick walls stronger?
Not necessarily. Thick walls can create sink, voids and warpage; ribs and better geometry may improve strength more efficiently.
What causes sink marks?
Sink marks are often caused by thick sections cooling and shrinking more slowly than surrounding walls.
Can wall thickness be changed after tooling?
Sometimes, but major wall changes are much easier before mold manufacturing.
Can CKMOLD review wall thickness?
Yes. CKMOLD can review CAD files and drawings for thin-wall or thick-wall molding risk.
Review Wall Strategy Against Material and Function
A part-specific DFM analysis should relate nominal walls and transitions to flow length, stiffness, cosmetic zones, gate access and the selected resin rather than applying one generic wall rule.