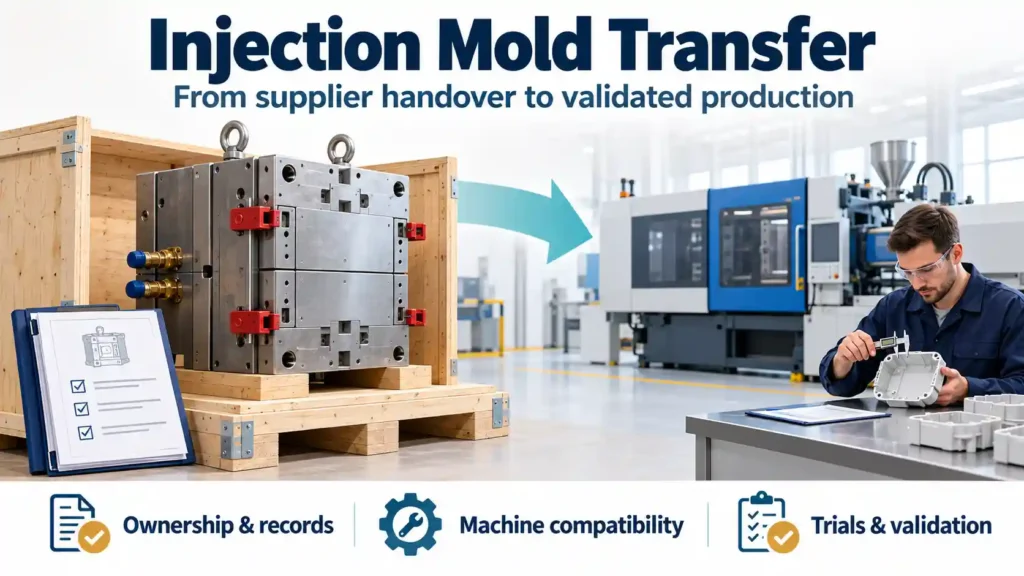
A mold transfer is a controlled engineering and logistics project, not simply a shipment. Verify ownership and release terms, preserve the current production baseline, confirm the receiving press and utility interfaces, document condition before transport, then run an incoming trial and the validation required by the customer.
The main risks are an incomplete handover, hidden wear, machine incompatibility and rushed approval while safety stock is running down. The following workflow separates the legal/commercial release, physical move, incoming condition check and production requalification.
Confirm that you own the mold.
Start with the purchase order, tooling agreement and payment record. Confirm who owns the identified mold, when title transferred, which release conditions apply, whether any agreed balance remains, what documentation is included and who pays for preservation, packing, transport and import work. Buyer ownership may support a transfer request, but the contract and applicable law determine the actual release rights and obligations.
When tooling costs are amortized into the part price, ownership and release conditions depend on the contract. If the agreed purchase volume has not been fulfilled, confirm whether any unrecovered tooling balance or other agreed charges must be settled before transfer.
If a supplier delays delivery of a mold that the buyer has paid for in full, raise the delay with the supplier directly and ask for a clear release date. This is worth sorting out face to face before you bring lawyers in, but don’t leave it ambiguous. Get it in writing that the mold will be released.
Gather your mold documentation package.
The documentation package is part of the transfer. Without current drawings, maintenance history, process records and approved samples, the receiving molder must reconstruct the baseline before it can judge whether the tool or the new process caused a difference.
Original 3D Mold Design & 2D Part Drawing (including the latest revision); location of gates, layout of runners, diagrams for cooling channels, and ejection details. Technical details of steel type and hardness for core and cavity. Documented accumulated shot count, the original agreed mold life, the maintenance history, and a current condition assessment. The latest production run and the last dimensional inspection report (CMM or other agreed measurement data) are complete. Process parameters: barrel temperature, injection pressure, hold time, cooling time, and cycle time. Material characteristics such as resin grade, color, and approved alternatives. All mold changes, repairs, and/or component replacements.
With a supplier such as CKMold, this documentation can be included in the project deliverables, depending on the agreed project scope. Annotated design documents from the mold design process can then track the tool throughout its life. Not all suppliers are as organized, so get your files ready early.
Assess the condition of mold.
If you are sending a mold to a new manufacturer, you must know what shape the mold is. You’re in a different position with an 800,000-shot mold than with a 200,000-shot mold.
Request the current supplier to provide the most up-to-date maintenance log. Examine parting line surfaces, gate areas, ejector pins, and cooling channels. Surface wear on the cavity side is evident from changes in part finish quality. Ejector pins wear out and/or get stuck in the workpiece. Obstruction or corrosion in cooling channels increases cycle times and causes warpage.
It’s easier to identify the need for refurbishment before transfer than after. You can determine this during incoming inspection by the receiving manufacturer, but consider scheduling a new gate insert or new ejector pins in your timeline and budget. Repair work needs an assessment of the mold and a separate quotation. If the degree of wear is severe enough to warrant a new tool, the CKMold injection mold cost calculator can help you budget for a replacement mold.
Build safety stock before you move anything.
Build the production-gap schedule from the real activities: final run and safety-stock build, release, preservation and crating, transport/customs, incoming inspection, interface work, repairs, benchmark trial, measurement and customer validation. A fixed two-week or two-month estimate is not reliable before these items are known.
Build up enough finished parts in stock before the transfer. Determine your consumption rate in the time frame you are planning to transfer into and allow for any buffers. Allow additional safety stock if repairs or refurbishment could extend the production gap.
This is the only step the purchaser is most likely to miss, as it requires planning while the current supply agreement is still in effect. Do it anyway. When you run out of parts during the transfer, you are under pressure to rush the validation from the new supplier, and that’s when quality issues begin.
Coordinate the physical move.
Injection molds are heavy precision tools whose machined and fitted surfaces, cooling circuits and moving components must be protected from impact, contamination and corrosion. Use the measured tool weight, lifting points, center of gravity and preservation/transport instructions to design the crate and handling plan.
Clean, dry, and rust-prevent all machined surfaces before leaving the facility. Cooling channels need to be blown out and treated. Slides, lifters, and other moving components should be secured according to the mold’s transport procedure. Any necessary disassembly should be performed, documented, and protected by qualified personnel. The mold must be secured and positioned on a pallet or crate to support the weight.
Customs papers will also be required for international transfers. When moving a mold from a Chinese supplier to a domestic facility, as well as from one country to another, confirm the HS code, arrange for shipping insurance for the replacement cost of the mold and clarify who pays the import duties. Agree on the Incoterms rule in advance. Under FOB, which applies to sea or inland waterway transport, risk generally passes to the buyer once the mold is loaded aboard the nominated vessel at the named port of shipment. For containerized or multimodal shipments, FCA may be more appropriate.
Have the current supplier take pictures of the mold before it is crated, including the parting line surfaces, runner system, and places of visible wear. These photographs will serve as the standard for the receiving inspection.
What the receiving manufacturer should do at intake
Upon arrival of the mold at the new facility, the mold must be subjected to a defined intake process and not be directly fed to a press. The receiving manufacturer checks the steel condition, cooling channel flow, fit of any moving parts and any shipping damage to the mold against the documentation package.
The next step is an incoming benchmark trial. Trial names such as T0 or T1 vary by supplier, so define the run by purpose, material, machine, quantity, cavity coverage and measurements instead of relying on the label. Historical settings are a reference; the receiving molder must establish settings suited to its press, auxiliary equipment, material handling and cooling.
CKMold reviews the transferred mold’s condition, available documentation, and compatibility with the receiving equipment before trial molding. Any required repairs or interface modifications are assessed and agreed before work proceeds. For details, see CKMold’s mold transfer service.
Check and validate parts against the original specifications.
The benchmark trial is a trial that informs you whether the mold works or not. Validation will tell you whether parts are suitable for manufacturing. These are two different questions.
Conduct a first article inspection (FAI) on parts from the new facility. Measure critical dimensions on the new parts, rather than relying on the previous report from the old supplier, and compare them to the tolerance specifications. Inspection methods, sampling, and cavity coverage should follow the agreed validation plan. Inspect surface finish, gate vestige, flash, sink marks, and cosmetic specifications, and include assembly and functional checks where applicable.
This is higher for regulated industries. For automotive programs under IATF 16949, a change in manufacturing location usually requires customer notification, approval, and PPAP resubmission, so confirm these requirements with your customer before relocating the mold. Your quality system may require a formal change notification for medical device work under ISO 13485. If requalification is not required for your industry, carry out any capability studies (such as Cpk) for your critical dimensions according to the agreed validation plan before releasing production.
Do not approve production because of only a few good trial run parts. Run parts at production speed, with the quantity, sampling, and cavity coverage set by the agreed validation plan, to gather the data needed to assess repeatability.
Common problems during mold transfers and how to avoid them
The top problem is machine compatibility. The mold was constructed for one manufacturer’s press, and the new manufacturer’s equipment is different from it. Compatibility depends on the clamping force the mold requires, shot capacity, mold dimensions and thickness, tie-bar spacing, opening and ejection travel, and interfaces such as the locating ring and nozzle. A nozzle-radius mismatch is a sealing and compatibility issue: the nozzle may not seal properly against the sprue bushing, which can cause leakage. Check machine specs with the receiving manufacturer prior to mold shipment.
Hot runner systems can cause problems if the new facility uses a different controller or if the connector configuration varies. Send the Hot Runner documentation to the receiver ahead of time, including the wiring diagram and controller model.
Facilities often vary in how they cool their hookups. The number of circuits, connector size, or flow rates could differ from the new facility. You can use adapters, but someone will need to map out the circuits before that mold hits the ground.
Process parameter gaps occur when there is inadequate documentation or when the old supplier used undocumented process parameters in the mold run. That’s why benchmark trial data is more important than a parameter sheet. The new manufacturer will likely need to create a process optimized for their equipment, so this can take time.
Cosmetic changes can surprise buyers even when dimensions are in spec. Surface gloss or color may vary slightly due to a different press, water temperature, or a different batch of resin. Set appearance acceptance criteria, using reference samples, before transfer.
Frequently asked questions
What is the average transfer time for a mold?
There is no reliable average transfer time. Build the schedule from release and export work, transport, incoming inspection, interface modifications, repair, trial, measurement, required PPAP or other requalification, and customer approval. Record dependencies and contingency rather than quoting a generic four-to-twelve-week range.
Is it possible to transfer a mold from a foreign supplier to a domestic producer or the other way around?
Yes. International mould transfers happen often. The logistics are more complex (customs, duties, longer shipping times, risk of corrosion during ocean freight), but the procedure is identical. Properly preserve the mold for transportation and insure it for replacement value.
Who is responsible for the mold refurbishment following a transfer?
Responsibility depends on the cause of the wear or damage, any warranty, the maintenance obligations, and the terms agreed in the original PO. If the mold is damaged as a result of poor maintenance by the previous supplier, the buyer may have a claim against that supplier. Repair work requires an assessment and a separate quotation.
What if the mold is damaged during shipping?
Shipping insurance protects equipment during transportation. Take photos of the mold before it leaves the old facility and as soon as it arrives at the new facility. File claims promptly with the carrier and the insurer.
What about a new PPAP or validation following a mold transfer?
For automotive work, confirm customer notification, approval, and PPAP resubmission requirements with your customer before relocating the mold. For other industries, consult your quality system requirements. It’s good practice to run a validation batch at the new facility even if it isn’t required.
Mold transfer checklist:
Before shipment
☐ Verify in writing that you own the mold, and confirm payment obligations, release conditions, and who pays the transfer costs.
☐ Gather the paperwork: 3D/2D drawings, steel specs, accumulated shot count, original agreed mold life, maintenance history, process parameters, and inspection data.
☐ Assess the mold’s physical condition and get a separate quotation for any repairs it needs.
☐ Check machine compatibility with the receiving manufacturer.
☐ Establish safety stock to cover the production gap.
☐ For automotive programs, confirm customer notification, approval, and PPAP resubmission requirements.
During the move
☐ Clean the mold and cover it with rust preventive.
☐ Secure slides, lifters, and other moving components according to the mold’s transport procedure.
☐ Take pictures of the mold before crating.
☐ Make shipping arrangements, agree on the Incoterms rule, and arrange the appropriate insurance.
At the new facility
☐ Inspect the mold on arrival and document its condition.
☐ Run a benchmark trial, using the historical process parameters as a reference.
☐ Do first article checks against the original specification, including assembly and functional checks where applicable.
☐ Run a pilot batch according to the agreed validation plan.
☐ Obtain customer approval before moving to production.
About CKMold
CKMOLD’s mold-transfer service covers the agreed intake, compatibility review, condition assessment and trial scope. Request the deliverables in writing; certification scope, documentation and production validation remain project-specific.
The CKMold injection mold cost calculator provides a rough cost estimate before requesting a formal quote. In contrast, the injection molding capabilities page provides machine tonnages, compatible resins, and industries served.