
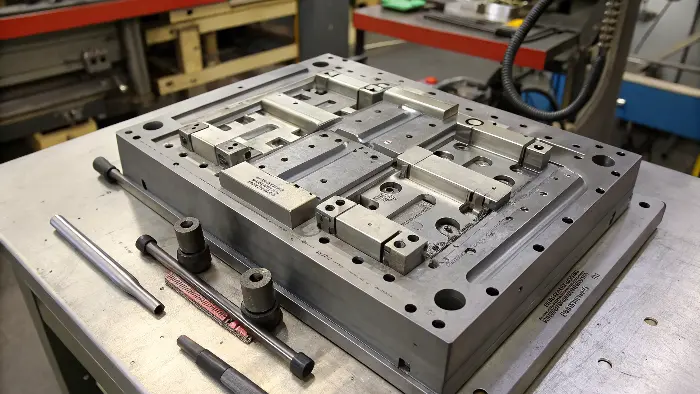
An injection mold slider is utilized during the injection molding process. It is utilized to create evenness and uniformity in the end product.
Without it, the process would be cumbersome and time-consuming.This blog will explain what an injection mold slider is and how it is utilized in the plastic injection molding process!
An injection mold slider is a side-action mechanism that moves a core feature out of the part before ejection. Sliders can create windows, hooks, ribs, threads, holes and other undercuts, but they add movement, shutoffs, wear surfaces, lubrication, timing and maintenance. The best slider is the simplest mechanism that releases the part reliably over the mold’s production life.
Related CKMOLD resources: mold design services, mold repair or modification, mold testing and validation.
Sliders and lifters are two ways to form undercuts; they are not automatically the best solution. First consider redesign, parting-line shutoffs, collapsible/unscrewing mechanisms, inserts or secondary operations, then select the mechanism from release direction, stroke, load, witness, cycle and service needs.
Design the Slider From Motion, Load and Locking
A slider is a guided, locked and serviceable load-bearing system. Define the undercut release direction and stroke first; then calculate pressure-loaded area, motion force, lock/support load, travel timing, return/retention, cooling, lubrication and sensing. A standard 15–25° angle-pin range is not a design rule. Start with the undercut mechanism-selection guide, then use the slider force calculation for the selected action.
DME describes angle pins as actuators typically used with a separate slide-retainer arrangement and requires the mold maker to fit and anti-rotate its insert. HASCO publishes slide-unit load data and the screening relationship F [N] = area [mm²] × pressure [bar] × 0.1. Review the DME angle-pin scope and HASCO slide-unit data, then apply the selected component manufacturer’s limits.
| Design record | Question it must answer |
|---|---|
| section and stroke stack | Does the core clear the feature before ejection? |
| load and lock calculation | What resists cavity pressure and where is it supported? |
| guide/wear map | Which replaceable surfaces control alignment and clearance? |
| sequence/sensing | How is safe return proven before mold closing? |
| service plan | Can cooling, lubrication and wear parts be maintained? |
Select Materials by Slider Component Duty
Do not assign P20, H13 or S7 to an entire slider from a fixed shot-count table. The contour insert, body, gib, wear plate, heel and angle pin have different hardness, toughness, bearing, corrosion, polish and repair needs. Review resin/filler, temperature, pressure load, sliding speed, lubrication restrictions, cooling and expected maintenance.
A supplier may offer different slide materials, heat treatments or low-friction coatings. Record the exact option and rated duty; a coating cannot correct poor support, misalignment, contamination or insufficient bearing area.
Record supplier/grade, heat treatment, target hardness where relevant, finish/coating, mating material, clearance and replacement method for each wear component.
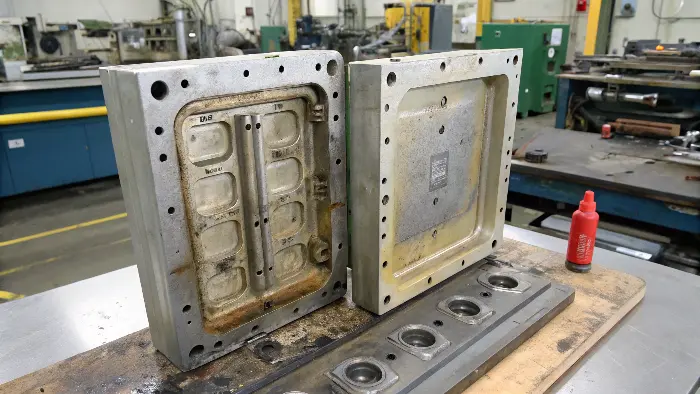
The Design and Working Principle of the Injection Mold Slider
Injection mold sliders are essential for creating complex plastic parts with side features or undercuts and for these details that a standard two-plate mold can’t release. We need to understand how these sliders are constructed and how they operate is crucial for ensuring reliable, efficient molding and high-quality finished products.
A typical injection mold slider system is made up of several interdependent parts, each serving a specific role in the mechanism:
Slider Body
The main moving block that travels laterally within the mold. It holds the cavity surface that forms the side feature (such as a hole or slot) on the molded part.
Angle Pin (Wedge or Horn Pin)
This is the heart of the slider mechanism. The angle pin is fixed at an angle and translates the vertical movement of the mold opening and closing into the horizontal motion of the slider. Its precise angle is critical for smooth operation and longevity.
Guide Rails or Grooves
These ensure the slider’s path is accurate and repeatable. They prevent misalignment, sticking, or binding during the slider’s travel.
Locking Heel or Locking Block
When the mold is closed, the locking heel engages with the back of the slider, holding it firmly in place against the high pressure of injection. This prevents the slider from being pushed back and causing defects like flash.
Return Mechanism
After the mold opens and the part is ejected, a return spring or pull pin resets the slider to its starting position, ready for the next cycle.
Wear Plates
These are inserted between the slider and the mold base to reduce friction and wear, extending the lifespan and maintaining precision.
Stopper Bolt or Travel Limit
This component defines the maximum stroke of the slider, preventing over-travel and potential damage.
How the Slider Works: Step-by-Step Sequence
The operation of an injection mold slider is a carefully choreographed mechanical process:
Mold Closing
As the mold closes, the angle pin enters the hole or groove in the slider. The sloped surface of the pin pushes the slider sideways, positioning it to form the undercut or side feature in the mold cavity.
Plastic Injection and Cooling
Molten plastic is injected into the cavity, filling all features—including those formed by the slider. The part cools and solidifies around the slider.
Mold Opening and Slider Retraction
When the mold opens, the angle pin is withdrawn. Its angled surface causes the slider to move laterally away from the molded part, freeing the undercut or side feature. This allows the part to be ejected without damage.
Slider Reset
Once the part is ejected, the return mechanism (spring or pull pin) moves the slider back to its original position, ready for the next molding cycle.
How the Components Work Together
The effectiveness of an injection mold slider depends on the precise interaction of its components:
-
The slider body and guide rails ensure smooth, accurate travel.
-
Wear plates and proper lubrication minimize friction and extend tool life.
-
The return mechanism helps support that the slider is correctly positioned for each cycle.
Durability and Maintenance
Because sliders operate under high loads and repeated cycles, their surfaces are often heat-treated (e.g., nitrided) to increase hardness and reduce wear. Regular maintenance—including cleaning, inspection, and lubrication—is essential to prevent issues like sticking, galling, or misalignment, all of which can cause costly downtime or part defects.
A clear understanding of the construction and working principle of injection mold sliders empowers you to design, operate, and troubleshoot molds for even the most complex part geometries. By ensuring that each component is properly specified and maintained, you can achieve consistent, high-quality production and avoid common pitfalls in the molding process.
Choreographing the Mechanical Dance
Designing a multi-action slider system requires precision timing and thinking in four dimensions (the three spatial dimensions plus the sequence of movement). One small miscalculation in the cam path can cause a catastrophic crash inside the mold.
Here’s how the two main approaches work:
- Slider-Activating-Slider:
- How it works: A primary, larger slider (Slider A) is actuated by a standard angle pin or hydraulic cylinder. A cam track is machined into the side or top of Slider A. A follower pin on a secondary slider (Slider B) sits in this track. As Slider A moves, the cam track forces Slider B to move in a different, often perpendicular, direction.
- Best for: Creating features on two different faces of a part where the movements need to be reliably synchronized.
- Critical element: The design of the cam track is paramount. The angles and radii must be smooth to ensure fluid motion without binding or excessive wear.
- Two-Stage Sliders (using Dog-Leg Cams):
- How it works: This is used when a slider needs to move in two different directions, like inward and then sideways. The slider itself has an L-shaped slot (the “dog leg”). The first angle pin moves it in one direction. As the mold opens further, that pin leaves the slot, and a second angle pin engages the other part of the L-shaped slot, pulling the slider in a second direction.
- Best for: Forming a feature that is itself “hooked” or has a complex shape that can’t be cleared with a single linear pull.
-
Critical element:The transition point in the dog-leg cam must be reliably smooth, and the timing of the pin engagement is everything. System Pros Cons Slider-Activating-Slider – Can create very complex, synchronized movements.
– Allows for compact mold designs.– Complex to design and machine.
– Higher risk of failure if not engineered reliably.
– Can be difficult to troubleshoot and repair.Two-Stage Sliders – Solves problems for “un-moldable” hooked features.
– Conceptually simpler than a slider-on-slider design.– Requires a very long mold open stroke.
– The dog-leg cam slot is a point of high stress and potential wear.For a business owner, the takeaway is this: if you have a complex part, don’t let a mold maker tell you it’s impossible without a thorough review. A skilled designer with experience in multi-action systems can often find a clever solution that saves you from having to compromise your product design or move to a more expensive multi-part assembly. This is where true molding expertise shines.
Troubleshoot Slider Problems by Evidence
- Contain: stop if return, lock or mold protection is uncertain; identify cavity and cycle.
- Inspect contact: witness/flash, shutoff, heel contact, guide marks, galling, debris and lubrication.
- Verify sequence: stroke, return, sensor, ejector/robot clearance and closing timing.
- Check load and temperature: pressure basis, support deflection, cooling flow and thermal growth.
- Measure wear: compare clearance and component dimensions with the as-built record.
- Correct and repeat: validate at the approved process window, not only by hand cycling.
For a production tool, request an as-built section, spare/wear list and maintenance interval. Use mold repair and modification when a load, alignment or worn-steel issue cannot be closed by normal service.
What a Slider Must Accomplish
The slider forms a lateral feature, remains locked during injection, moves after mold opening or through an angle, clears the part and returns to a repeatable position. Its design must account for cavity pressure, friction, wear, ejection sequence and access for inspection.
Common Slider Architectures
Angle pins can drive a slider during mold opening, while hydraulic or pneumatic cylinders provide controlled independent movement. Wear plates, guide rails, wedges, return stops and locking surfaces support the motion. The appropriate architecture depends on stroke, timing, force, space and cycle.
Locking and Shutoff Protect Quality
A slider may move easily and still fail under injection pressure if the locking wedge or shutoff is weak. Positive locking, suitable contact, steel hardness and support behind the core feature prevent flash and movement. Shutoff geometry should be inspected after repeated cycles.
Wear, Lubrication and Cooling Matter
Sliding surfaces, angle pins, bushings and wear plates require suitable clearance and lubrication. Abrasive resin, heat, contamination and poor maintenance accelerate wear. Cooling near the slider may need special routing, and hoses or fittings must not limit movement.
Validate Timing and Service Access
Trial the slider through open, core-pull, eject and return sequences. Check flash, marks, interference, noise, lubrication, temperature and repeatability. The design should allow a technician to inspect, clean, replace wear plates and adjust timing without dismantling the entire mold.
Injection Mold Sliders: Buyer Review Checklist
- Define undercut, stroke, direction, timing, force, space and ejection requirements.
- Choose angle-pin, hydraulic, pneumatic or other drive from the actual motion need.
- Design positive locking, shutoff support, wear surfaces, guides and return control.
- Plan lubrication, cooling, contamination protection and service access.
- Validate motion, flash, marks, interference, timing and maintenance after trials.
FAQ
When is a slider needed in an injection mold?
It is needed when a side feature cannot release in the main mold-opening direction and the part design cannot be changed to remove the undercut.
Are hydraulic sliders better than angle-pin sliders?
They offer different timing and force control; the better choice depends on stroke, cycle, space, cost, maintenance and control requirements.
Conclusion
From simple design concepts and material choice to sophisticated multi-functional systems and fault detection, sliders are a must. They’re not simply mold components; they’re enablers of innovative product design. You get them correct and you have quality, efficiency, and profitability for your company. Don’t miss these key facts