
Struggling with complex mold designs? This can lead to costly errors and project delays. This guide will simplify the essentials for you.
A design-to-manufacturing handoff gives the toolroom, purchaser and trial team a controlled set of drawings, BOM items, interface requirements and acceptance decisions. The package should make revisions and unresolved issues explicit before machining or procurement begins.
Understanding these key areas is fundamental for anyone in this field, from product designers to seasoned manufacturing professionals. I’ve spent years in this industry, starting on the factory floor and later building my own mold and CNC trading company. I’ve seen firsthand how a solid grasp of these principles can make or break a project. My goal with CKMOLD is to share this knowledge, helping you navigate the complexities and achieve success. So, let’s dive into what makes a great mold design.
Release a Controlled Design-to-Manufacturing Package
The handoff should let the toolroom, purchaser and trial team work to the same approved revision:
| Deliverable | Required decision or verification |
|---|---|
| Part CAD and 2D drawing | Units, revision, datums, critical dimensions, surface zones and permitted deviations |
| Mold assembly and detail drawings | Actions/clearances, shutoffs, cooling, ejection sequence and manufacturing tolerances |
| BOM and material specifications | Exact components, steel grade, heat treatment/hardness, wear surfaces and replacement items |
| Receiving-equipment interfaces | Mold/press fit, connections, power/thermocouples, actuation, utilities and lifting/handling requirements |
| Trial and acceptance plan | Resin grade, sample/measurement conditions, reports, release criteria and open-item ownership |
| Change control | Approved revision, impact on bought-out parts, schedule and acceptance; no uncontrolled drawing substitutions |
Check the selected hot runner’s interface and control scope and specify evidence for claimed process benefits. For complex parts, keep deformation and ejection risks on the release/open-item list.
Use the relevant equipment/component supplier instructions, such as Husky’s system manuals, for actual interface and installation requirements; a generic checklist does not replace the selected system manual. Resolve incompatible connections before the mold reaches the receiving press.
This is the release package, distinct from DFM financial prioritization and the build milestone schedule. For a design/build enquiry, identify which documents already exist and which decisions remain open; send controlled design files to jerry@ckmold.com after submitting the form.
Record the Process Assumptions That the Toolroom Must Preserve
Link the proposed filling, packing, cooling and ejection sequence to the released mold drawings. Identify the features that depend on resin behavior or trial confirmation, the permitted adjustment direction and who can approve a change.
Carry the Approved Material Specification Into the Release Package
Identify the exact resin grade, color or filler specification, supplier document revision and expected conditioning state. Record unresolved material choices before steel release because a substitution can change flow, shrinkage, surface behavior and the acceptance basis.
-
What Makes Design for Manufacturability (DFM) a Game-Changer in Mold Development?
Are your innovative part designs proving difficult or expensive to mold? This often inflates costs and extends timelines unnecessarily. DFM principles are your practical solution.
Design for Manufacturability (DFM) is a critical proactive approach. It involves designing parts to be as easy and economical to mold as possible, right from the start. This minimizes defects, reduces cycle times, and lowers overall production costs.
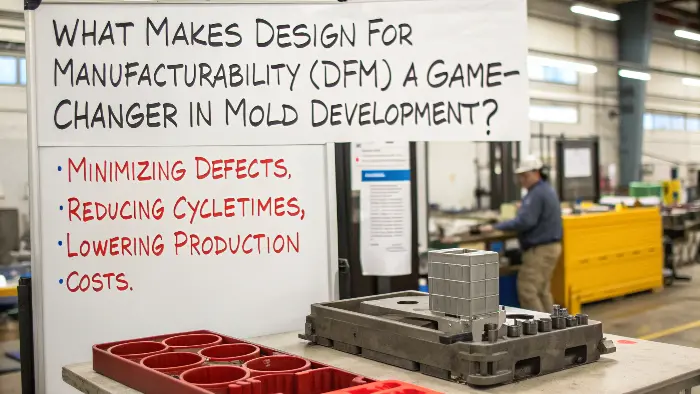
DFM isn’t just a buzzword; it’s a foundational philosophy in modern manufacturing. As a designer or engineer, incorporating DFM principles means you’re thinking about the manufacturing process while you’re still in the design phase. This collaboration between design and manufacturing perspectives is where the magic happens. I’ve seen too many brilliant designs fail or become excessively expensive because basic DFM rules were ignored.
Core DFM Principles for Injection Molding
When I review a design for moldability, these are some of the first things I look at:
- Uniform Wall Thickness: This is perhaps the most important rule. Consistent wall thickness helps prevent issues like sink marks, warping, and voids. Molten plastic flows more evenly and cools more uniformly. If varying thicknesses are unavoidable, the transition should be gradual.
- Draft Angles: These are slight tapers applied to the vertical walls of the part, in the direction of mold opening. Typically, 1 to 2 degrees is sufficient for most surfaces, but textured surfaces might need more. Draft angles allow the part to be easily ejected from the mold without drag marks or damage.
- Radii and Corners: Sharp internal corners are stress concentrators and can make mold filling difficult. Generous radii on both internal and external corners improve material flow, reduce stress, and increase the strength of the part. They also make the mold easier to machine and more durable.
- Ribs and Bosses: Ribs can be used to increase stiffness and strength without increasing overall wall thickness. Bosses are typically used for mounting or alignment. Both should follow DFM guidelines (e.g., rib thickness around 50-60% of the adjoining wall, height limits, draft angles).
- Undercuts: These are features that prevent the part from being directly ejected from the mold, like a side hole or a snap-fit latch. While sometimes necessary, they add complexity and cost to the mold, often requiring side-actions or lifters. DFM aims to minimize or cleverly design undercuts if they are unavoidable.
Implementing DFM isn’t about restricting creativity; it’s about channeling it in a way that’s practical for production. The benefits are significant: reduced tooling costs, faster production cycles, higher quality parts, and fewer headaches for everyone involved.How Can You Optimize Critical Mold Design Elements for Peak Production Efficiency?
Are your current molds leading to inefficient production cycles or inconsistent part quality? This often means slow output and higher per-part costs. Optimizing your mold design is the key to improvement.
Optimizing critical mold design elements like the gating system, cooling channels, and venting strategy is absolutely essential for achieving peak production efficiency. A well-designed mold minimizes cycle times, reduces part defects, and extends the operational life of the tool.
Once you have a part designed with DFM principles in mind, the next step is to design the mold itself. This is where a deep understanding of how plastic flows, cools, and ejects becomes paramount. I’ve worked on many molds over the years, and the difference between a merely functional mold and a highly optimized one is often found in the details of these critical elements. An optimized mold doesn’t just make parts; it makes them quickly, consistently, and cost-effectively.
Optimizing Gate Design and Location
The gate is the opening through which molten plastic enters the mold cavity. Its design and location are critical.
- Types of Gates: There are many types, including edge gates (simple, on the parting line), submarine (or tunnel) gates (de-gate automatically during ejection), hot runner gates (keep plastic molten right up to the cavity, reducing waste and cycle time but adding cost), and direct sprue gates (for single-cavity molds). The choice depends on the part material, geometry, cosmetic requirements, and production volume.
- Impact of Gate Location: The gate should be placed to ensure complete and balanced filling of the cavity. It should ideally be located in the thickest section of the part to allow for proper packing. Poor gate location can lead to weld lines, air traps, jetting, or warpage. It also affects the cosmetic appearance, as a gate mark will be visible.
Designing Effective Cooling Systems
Cooling typically accounts for the largest portion of the injection molding cycle time.
- Importance of Cooling: Efficient and uniform cooling is vital for minimizing cycle time and controlling part quality (e.g., preventing warpage and ensuring dimensional stability).
- Cooling Channel Design: Channels should be designed to provide even cooling across the part surface. They should be placed as close to the cavity surface as possible without compromising mold strength. The diameter and layout of the channels are important, and sometimes conformal cooling (channels that follow the contour of the part) is used for complex geometries.
The Role of Venting
As molten plastic fills the cavity, the air and any gases generated from the plastic must escape.
- Why Venting is Needed: Inadequate venting can lead to trapped air, resulting in incomplete filling (short shots), burn marks (from compressed, superheated air), or poor surface finish.
- Common Venting Strategies: Qualify parting-line, insert and ejector vent paths for the actual resin and local filling conditions. Document the approved gate, cooling and vent details and any steel-safe trial allowances. A proposed cycle improvement needs a stated baseline and measured trial comparison; retain open issues until the agreed evidence supports release.
Conclusion
Release a consistent drawing, BOM and acceptance package, then control changes against that revision. Close interface conflicts and record the remaining trial decisions so the manufactured tool can be checked against the approved design.