
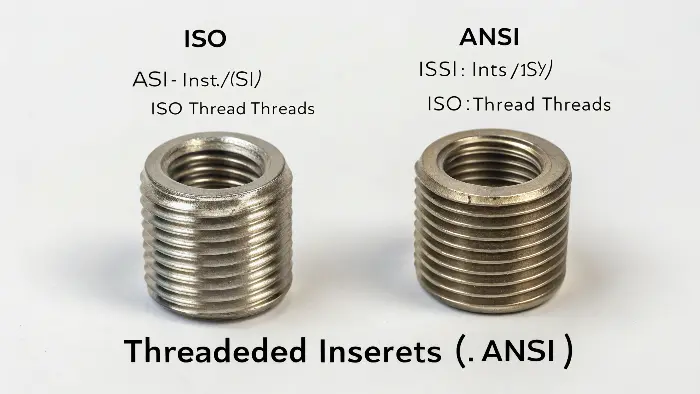
Insert molding is more cost-effective than separate assembly when the additional tooling, loading and process-control cost is offset by lower per-good-part assembly, inspection, handling and failure cost. It is not automatically cheaper. For low volumes, frequent insert changes or simple parts, post-mold heat, ultrasonic, press or self-tapping installation can remain the better economic route.
Compare both routes for the same part function, joint performance, cosmetic requirement and accepted quality level. Then calculate fixed cost, variable cost per accepted good part and the production quantity at which the cost lines cross.
When insert molding can reduce total cost
In insert molding, a metal or other component is located in the mold before plastic is injected around it. Placement may be manual or automated. The route can be attractive when:
- volume is high enough to recover the additional mold, fixture and automation cost;
- the insert geometry can be located repeatably and protected against movement or resin entry;
- the integrated joint meets pull-out, torque, sealing or electrical requirements without a later station;
- post-mold handling, installation and inspection are significant cost or capacity constraints;
- the design benefits from encapsulation, alignment or a captive component that is difficult to achieve later;
- insert supply, cleanliness and dimensional consistency are stable enough for the molding process.
The SPIROL Inserts for Plastics Design Guide distinguishes molded-in inserts from post-mold heat/ultrasonic, press-in and self-tapping alternatives. It notes that molded-in placement can cost more than post-mold installation while providing strong performance. That is a design trade-off, not proof that one process is always cheaper.
When separate assembly can remain more economical
- Low or uncertain demand: a simpler mold and a flexible assembly fixture may require less fixed investment.
- Many insert variants: installing the insert after molding can reduce tool changeover and wrong-insert risk.
- Insert supply is unstable: the molding cell should not sit idle because inserts are missing or out of tolerance.
- Defects can be recovered: a post-mold insert may be replaceable without scrapping the complete molded part.
- The required joint is readily achieved: heat or ultrasonic installation, press-in or self-tapping designs may meet the same torque and pull-out requirement at lower total cost.
- Automation is already available: an existing assembly cell can change the cost comparison materially.
The relevant comparison is not “insert molding versus manual labor” by default. It is insert molding versus the best practical post-assembly route that satisfies the same specification.
Use one cost model and one unit of output
Calculate both alternatives in the same currency and at the same production quantity:
Total route cost = fixed project cost + (variable cost per accepted good part × accepted quantity)
Fixed cost may include:
- mold construction and insert-retention features;
- assembly fixtures, insert-loading nests, sensors and guarding;
- robot or feeder integration allocated to the project;
- process development, validation and approved gauges.
Variable cost per accepted good part may include:
- resin, insert and other purchased components;
- machine occupation and molding conversion;
- manual or automated loading and assembly;
- inspection and functional testing;
- consumables, packaging between operations and work-in-process handling;
- the expected cost of scrap and rework.
Avoid double counting: if the variable rate is already expressed per accepted good part and includes expected scrap and rework, do not divide it by yield again or add the same scrap allowance in a second line. Use documented assumptions for uptime, cavities, labor burden and inspection frequency.
Break-even calculation
If insert molding has the higher fixed cost but the lower variable cost, the break-even accepted quantity is:
Break-even quantity = (insert-molding fixed cost − post-assembly fixed cost) ÷ (post-assembly variable cost − insert-molding variable cost)
If the post-assembly variable cost is equal to or lower than the insert-molding variable cost, there is no positive operating-cost payback under those assumptions. Insert molding could still be chosen for performance, alignment, sealing or supply-chain reasons, but the decision should not be described as a cost recovery.
Illustrative example — not a CKMOLD project or quotation
Assume the two routes produce the same accepted housing with the same threaded insert, torque requirement and cosmetic criteria. All values below are transparent demonstration assumptions in US dollars; they are not market averages.
| Cost item | Insert molding | Post-mold assembly |
|---|---|---|
| Fixed mold, fixtures and validation | $48,000 | $18,000 |
| Resin and molding conversion per accepted part | $0.70 | $0.65 |
| Insert per accepted part | $0.22 | $0.22 |
| Insert loading or post-mold installation per accepted part | $0.28 | $0.38 |
| Inspection per accepted part | $0.05 | $0.12 |
| Expected scrap and rework per accepted part | $0.05 | $0.13 |
| Total variable cost per accepted part | $1.30 | $1.50 |
The insert-molding route requires $30,000 more fixed investment and saves $0.20 per accepted part. The illustrative break-even is therefore:
$30,000 ÷ $0.20 = 150,000 accepted parts
- At 100,000 accepted parts: insert molding costs $48,000 + $130,000 = $178,000; post-assembly costs $18,000 + $150,000 = $168,000. Post-assembly is $10,000 lower.
- At 250,000 accepted parts: insert molding costs $48,000 + $325,000 = $373,000; post-assembly costs $18,000 + $375,000 = $393,000. Insert molding is $20,000 lower.
Before using this model, replace every assumption with supplier quotations, measured cycle and labor data, realistic yield and the accepted lifetime quantity. Run sensitivity cases for volume, insert price, loading rate and scrap because a small change in the $0.20 saving changes the break-even materially.
Quality and risk can change the economic answer
Insert position and retention
A molded-in insert must locate repeatably and withstand injection pressure without moving. The design must manage flash, resin entry into threads, insert orientation and safe loading. Sensors or vision may reduce missing-insert risk but add equipment and validation cost.
Joint performance
Specify torque, pull-out, push-out, electrical, sealing and environmental requirements. The SPIROL guide explains that insert diameter, length, knurls, grooves and plastic flow affect torque and pull-out performance. Use component testing on the selected resin and geometry rather than a generic process claim.
Failure location and recoverability
In insert molding, a misplaced or contaminated insert can scrap the insert and molded part together. In post-assembly, the base molded part may sometimes be inspected first and a faulty insert may be replaceable. The reverse can also occur: a robust molded-in joint may avoid downstream installation damage. Put the expected failure and recovery cost into the model.
Capacity and changeover
Manual insert loading can lengthen machine occupation and expose the molding cell to operator variation. Automation can improve repeatability, but feeders, grippers, nests, change parts and maintenance must be included. For multi-cavity production, confirm whether every insert can be presented and verified within the required molding cycle.
Decision table
| Condition | Route to evaluate first | Evidence needed |
|---|---|---|
| High stable volume; repeatable insert; costly downstream assembly | Insert molding | Loading study, cycle impact, yield plan, joint test and automation quotation |
| Low volume or uncertain forecast | Post-mold assembly | Fixture/labor quotation and proof that the installed joint meets the same requirement |
| Frequent insert variants or late configuration | Post-mold assembly | Changeover, traceability and mistake-proofing plan |
| Encapsulation, alignment or sealing is fundamental to function | Insert molding | DFM, insert-retention analysis and validation test |
| Insert delivery or dimensions are unstable | Resolve supply risk before committing either route | Incoming specification, capacity plan and nonconforming-material process |
Information needed for a comparable quotation
- 3D model, drawing and exact resin grade;
- insert drawing, material, plating and dimensional tolerances;
- annual, launch and lifetime accepted quantities;
- required torque, pull-out, sealing, electrical and cosmetic tests;
- allowed installation methods and whether automation is required;
- target cavity count, available molding machine and production location;
- inspection level, traceability, packaging and replacement policy;
- separate fixed and per-good-part cost for both routes.
Use insert molding and overmolding DFM to review retention, shutoffs, loading and resin flow, and compare the result with the most appropriate post-assembly method. For production assumptions, see production injection molding.
Use our injection mold cost estimator for a preliminary tooling budget, then request an engineering review of cycle time, yield and production cost. A final decision requires part-specific quotations and validation, not a generic break-even number.