
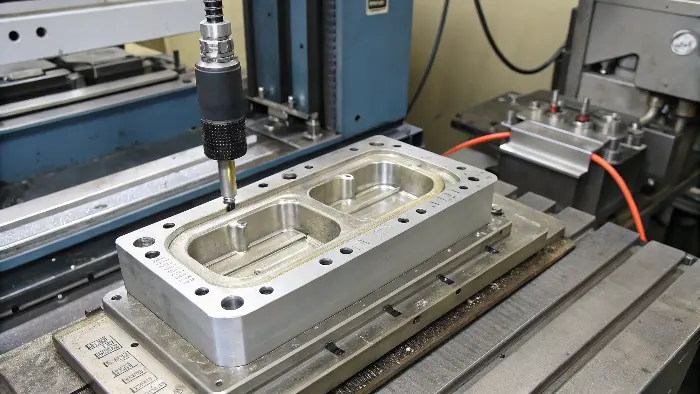
Designing of complex parts that need both metal strength and versatility of plastics can prove to be a mess actually. The conventional operations of assembling tend to be very expensive, time-consuming as well as unreliable. Probably, you need a more built-in and resistant service.
Metal and plastic insert molding can create a compact component that uses each material for what it does best: metal for conductivity, threads, strength, wear or precision, and plastic for insulation, shape, sealing or lightweight integration. The process is powerful, but metal-plastic interfaces create risks from pressure, thermal expansion, corrosion, bonding, flash and stress.
Related CKMOLD resources: insert molding and overmolding, mold design, mold testing and validation.
Insert Molding is something that CKMOLD is able to offer as the ability to combine metal (such as threaded inserts, pins, contacts etc.) with other thermoplastics in one sweeping automated sweep. This produces sturdy, long lived and intricate components, minimising assembly time, and enhancing overall products quality in high tech applications, such as electronics and automobile components.
Confirm Insert-Molding Capability Against the Part
Insert molding capability must be confirmed against the specific insert, resin, geometry, cavity count, press and validation plan. Common inserts include threaded bushings, contacts, terminals, pins, stamped parts and electronic subassemblies, but each creates different loading, sealing, heat, alignment and test risks.
Provide insert drawing/material/plating, molded resin grade, interface tolerances, orientation, pull/torque/electrical/seal requirements, annual quantity and traceability. The supplier should return a DFM showing retention, shutoffs, loading, sensing, gate/flow, venting, cooling, protection of functional surfaces and reject handling.
Use the insert molding and overmolding scope to request a project review; no universal machine, accuracy or capacity claim is implied.
Build the Production Cell Around Loading and Verification
Horizontal, vertical or rotary-table machines may be suitable depending on insert loading, orientation, ergonomics, automation and mold architecture. The decision also requires shot/injection/clamp capacity, platen and mold fit, core-pull/robot/sensor interfaces, drying and temperature control.
Manual loading needs safe access, a positive nest and mistake-proofing. Automation needs feeders, grippers, presentation, reject recovery and confirmation that all inserts are present and seated before closing. Preserve insert lot and cavity identity when the product risk requires traceability.
SPIROL’s Inserts for Plastics Design Guide distinguishes molded-in from post-mold installation and discusses insert geometry/performance within its product scope. It does not prove a joint without testing the selected resin, insert and part.
Illustrative Engineering Scenario—Not a CKMOLD Customer Project
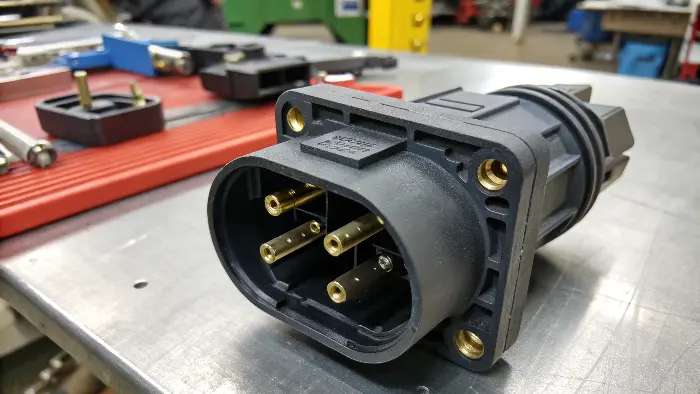
Assume a connector requires a plated terminal to remain aligned while resin flows around it. The engineering questions are whether the nest protects the contact surface, whether cavity pressure can move the terminal, where air and flash can escape, and how continuity/position will be inspected. A fixture study, insert-retention analysis and production-like samples are required before claiming sealing or reliability.
This scenario illustrates the method only. It is not a published CKMOLD project, customer result, hermetic-seal guarantee or evidence of a particular saving.
For projects that add automated loading, multiple inserts, electronics or a second material, the advanced insert-molding methods guide explains how to qualify handling, sensing, interface loads and the production cell without assuming automation is always justified.
Control the Insert-Molding Sequence
- Receive and verify insert material, plating, dimensions, cleanliness and lot identity.
- Load and positively locate the insert; confirm orientation and seating.
- Close only after the sensing/mistake-proofing condition is satisfied.
- Mold with a validated fill/pack/cooling sequence that does not move, overheat or contaminate the insert.
- Eject and handle without bending the insert or damaging the polymer interface.
- Inspect presence/position and the specified torque, pull, electrical, seal or functional result.
Do not assume chemical bonding. Retention may be mechanical, adhesive/chemical or a combination and must be demonstrated for the exact material surfaces and environment. Thermoplastic insert molding should not be confused with thermoset or rubber transfer molding, which uses a different material path and cure process.
Insert Molding Versus Polymer Overmolding
Insert molding places a pre-made component in the mold before resin is injected around or against it. Multi-material overmolding usually adds a polymer shot onto a previously molded or prepared substrate. Both need retention, shutoff, thermal/chemical compatibility and interface testing, but their loading, tooling and bonding questions differ.
For a quote, state whether the substrate is purchased, customer-supplied or molded in a first operation; define allowable handling damage, interface preparation, scrap ownership and tests. Submit the controlled specification through the RFQ page and send CAD separately to jerry@ckmold.com.
Assign the Function to the Right Material
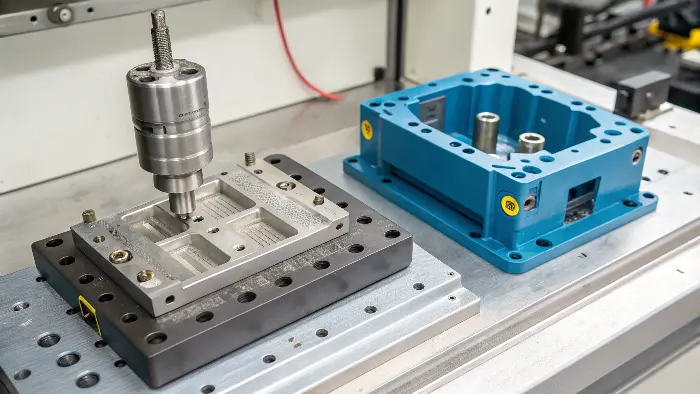
Define whether the insert carries load, current, torque, wear, heat, a seal or a datum. The plastic may provide insulation, protection, guidance or a secondary interface. This functional division determines coverage, retention, exposed surfaces, gate direction and inspection.
Design Retention Without Damaging the Insert
Knurls, holes, grooves, flats and undercuts can resist pull-out or rotation. The geometry should avoid cutting through a critical electrical or sealing feature and should remain formable, clean and locatable before molding.
Control Thermal and Chemical Compatibility
Metal and plastic may expand differently, and coating, oil, plating or cleaning can affect adhesion and corrosion. Resin temperature, insert preheat, mold temperature, cooling, barrier design and the final environment should be reviewed together.
Protect Functional Surfaces and Tolerances
Threads, contacts, magnet faces, bearings, seals and precision datums may need masking, shutoff, support or post-mold inspection. Flash on a non-visible electrical or sealing surface can be a serious functional failure.
Validate the Composite Component
Use pull, torque, rotation, electrical, insulation, leak, thermal, vibration, corrosion and aging tests appropriate to the application. Track insert lot, surface treatment, cavity and process so a failure can be traced to the correct source.
Combining Metal and Plastic With Insert Molding for Advanced: Buyer Review Checklist
- Define the structural, electrical, thermal, sealing, wear and assembly role of each material.
- Design retention, locating, support and coverage without damaging insert function.
- Review expansion, coating, plating, cleaning, corrosion, resin and temperature compatibility.
- Protect threads, contacts, bearings, seals and precision surfaces from flash and movement.
- Validate composite function with traceable insert, cavity, material and process records.
FAQ
What are common metal inserts in injection molding?
Threaded bushings, terminals, stamped contacts, shafts, bushings, magnets, meshes and precision hardware may be used, depending on the application.
How is metal insert movement prevented?
Use positive locating, support, anti-rotation features, suitable cavity contact, controlled filling and validated loading or automation.
Conclusion
CKMOLD’s insert molding capabilities, particularly for combining metal and plastic, offer a powerful way to create advanced, integrated components. By understanding our specific strengths in precision, material science, mold design, and process control, along with real-world applications and the nuances of the thermoplastic molding process, you can better leverage this technology for stronger, more reliable, and often more cost-effective products. We’re dedicated to helping you “Master Molding Right.”