
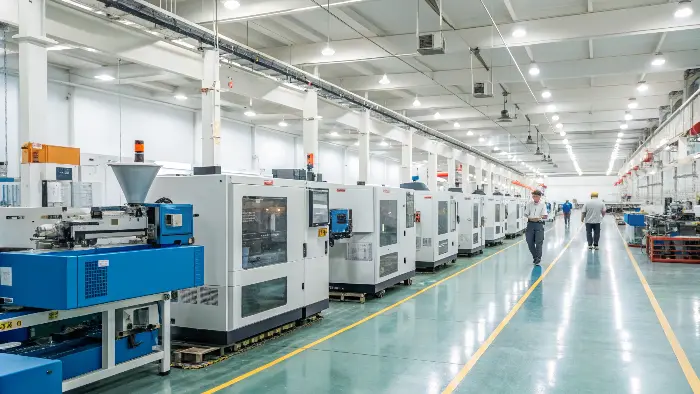
An injection mold is an assembly that shapes, cools and releases a polymer part. The cavity and core define the part geometry, while the feed system, vents, cooling circuits, guidance and ejection system support a repeatable molding cycle.
An injection mold is a reusable production system that forms molten polymer into a controlled shape, removes heat, releases the part and repeats the cycle. It includes more than the cavity outline: core, cavity, base, runner, gate, vents, cooling, ejection, side actions, sensors and maintenance features all contribute to the final part and its production cost.
Related CKMOLD resources: injection mold services, mold design, production injection molding.
Hot plastic is pumped into a mold via a sprue and flows into cavities via runners and gates. The mold is subsequently opened following the cooling process and the injection molding machine’s ejector rod forces the ejector plate of the mold to eject additional moldings.
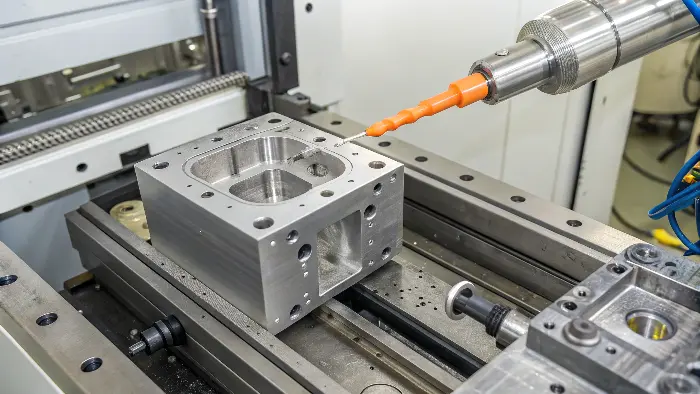
An injection mold is a specifically made instrument which is basically a hollow block of metal that contains a accurately shaped hole within it. It is typically made out of tough steel (e.g. P20 or H13). During the production procedure, hot plastic in liquid stain is pressured in large quantities into this hole. The plastic is then left to cool and become solid, acquiring the specific shape of the cavity. The mold is opened, and the complete part of plastic is extruded. The cycle enables the production of similar parts in a swift and repeat fashion, including a bottle cap and a car dashboard.
What Is The Core Meaning Of An Injection Mold?
When you hear the phrase injection mold you can imagine an uncomplicated metal box. What can this tool really mean in the manufacturing world? It is easy to underestimate the complexity of the matter, when you think of it too simply. You may also lose the very important connection between the design of the mold and quality of the final product along with its strength and finish. Suppose we get at its real meaning. An injection mold is not just a mold, it is actually the core of mass-production of plastic parts.
The essence of an injection mold is the fact that, it is your final product inverted or negative. Just think of making a jelly dessert; the jelly has a shape because of the mold. The same is done by an injection mold except an injection mold does so by using high tech plastics at extreme conditions. It is a highly engineered piece of steel, which holds the exact inverse geometry of what it is you are interested in making. It is intended to mold molten plastic using immense pressure and heat and create a solid repeatable product.
What an Injection Mold Actually Contains
An injection mold is a controlled production asset, not simply a negative cavity in a steel block. Core and cavity form the part, while the feed, venting, cooling, support, alignment, action and ejection systems determine whether the geometry can be filled, cooled, released and repeated safely.
Material selection is component-specific. A mold base, cavity insert, gate insert, slide and wear plate may need different strength, hardness, corrosion, polish, thermal and repair characteristics. Labels such as P20, H13 or stainless are not complete specifications and do not guarantee a fixed number of cycles. State the producer/grade, condition, heat treatment, component location and acceptance record.
Before steel release, the buyer should receive a mold concept showing parting, gates, cavities, actions, cooling, ejection, critical steel-safe areas and machine interfaces. The mold-design scope explains the decisions that should be closed before manufacturing.
How Can We Explain Injection Molding Simply?
The process can be explained as a controlled sequence: close and lock the mold, fill, transfer to packing, cool, open, release/eject and repeat. Each stage links the part, resin, mold, machine and acceptance evidence.
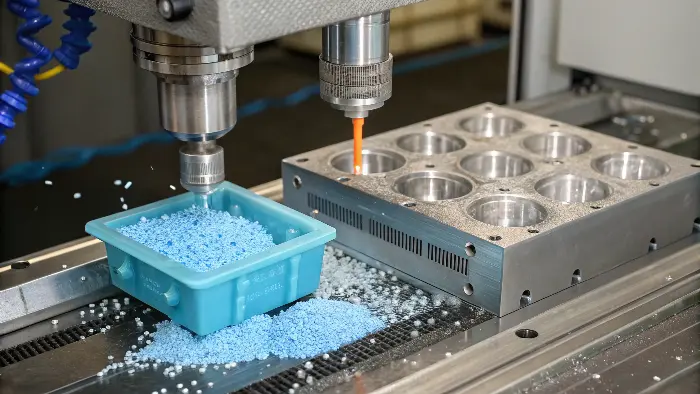
The simplest description of injection molding is that is resembles a high-powered automatic hot glue gun. The first step is a melting of tiny plastic pellets to make a hot liquid. This liquid plastic is then forcefully squirted or shot into a closed metal mold among another thing. The plastic is cooled by circulation of water around the mold and as such, the solidification process is very fast. The mold is lastly opened and the new part of plastic pushed out. All this runs again, and again, in a few seconds or a little more, to produce thousands or millions of exactly the same parts.
The Four Key Stages of the Injection Molding Cycle
While the analogy is useful, a professional like you needs to know the specific stages. The entire process is a finely tuned cycle. If any stage is off by even a fraction of a second, it can lead to defects. The cycle consists of four main stages that repeat seamlessly.
| Stage | Purpose | Critical Factors |
|---|---|---|
| 1. Clamping | The two halves of the mold are securely closed by the molding machine. | Clamping Force: Must be high enough to keep the mold shut against injection pressure. |
| 2. Injection | Molten plastic is forced from the injection unit into the mold cavity. | Injection Pressure & Speed: Controls how the part is filled. Too fast causes flash; too slow causes short shots. |
| 3. Cooling | The part solidifies inside the mold as heat is transferred to the mold. | Cooling Time: The longest part of the cycle. Determines cycle time and affects part shrinkage and warping. |
| 4. Ejection | The mold opens, and the ejector system pushes the solid part out. | Ejection Speed & Force: Must be controlled to avoid damaging or deforming the newly made part. |
Understanding these four stages is fundamental. As a designer, your choices directly impact each one. For example, a thick wall section in your design will dramatically increase the required cooling time, slowing down the entire production run and increasing the cost of every single part.
What Are The Key Components Of An Injection Mold?
You may know that a mold has a hole, but what about the rest of the parts that causes it to work? Learning all about the structure of a mold is essential in ensuring the designing of parts that can be produced in an efficient manner. By overlooking these additional elements, you will very easily design something that is hard to manufacture or one that causes typical defects in appearance such as sink marks, warping, or flash. Just to cut up a normal injection mold and see the key parts.
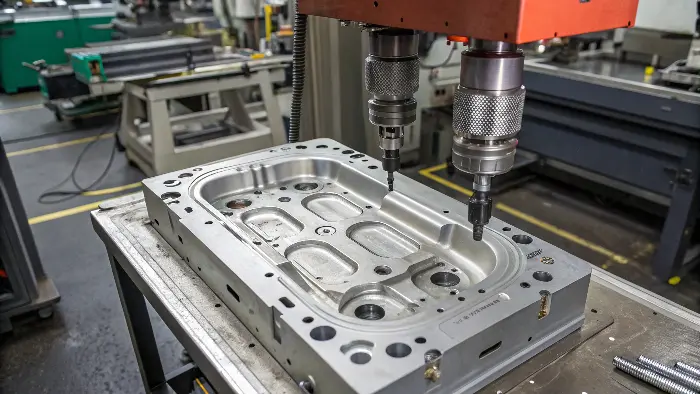
An injection mold is a complex assembly with several key systems. The two main halves are the A-side (or cavity side) and the B-side (or core side). Inside, you have the cavity and core, which come together to form the part’s shape. The sprue, runners, and gates create a pathway for the plastic to flow into the cavity. A cooling system of channels regulates the mold’s temperature. Finally, the ejector system, with its pins and plates, pushes the finished part out after it has cooled.
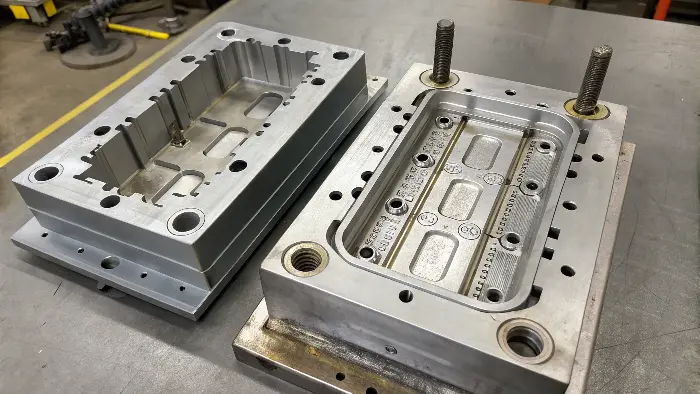
A mold is an assembly of precision systems rather than one block of steel. Reviewing an assembly section, bill of materials, flow path, cooling, ejection and side-action sequence helps a designer identify manufacturing and service risks before release.
The Two Halves: A-Side and B-Side
Every standard mold is split into two halves.
- The A-Side (Cavity Half): This half usually forms the exterior of the part, often the “show” surface that the customer sees. It’s typically mounted on the stationary platen of the molding machine. The main sprue bushing, where plastic first enters the mold, is on this side.
- The B-Side (Core Half): This half is mounted on the moving platen. It usually forms the interior features of a part, like ribs, bosses, and other functional elements. The ejector system is housed within the B-side, as this is the half the part sticks to when the mold opens.
The Systems That Make It Work
Beyond the two halves, the mold is organized into several critical systems. As a designer, you need to consider how your part will interact with each one.
| System Name | Components | Function | Design Consideration |
|---|---|---|---|
| Feed System | Sprue, Runners, Gates | Delivers molten plastic from the machine nozzle to the cavity. | Gate location is critical. It affects filling, part appearance, and de-gating. |
| Shaping System | Cavity, Core, Slides, Lifters | Forms the actual shape of the plastic part, including undercuts. | Requires draft angles for easy release. Complex geometry may need slides or lifters. |
| Cooling System | Cooling Channels, Baffles, Bubblers | Removes heat from the plastic, allowing it to solidify. | Uniform cooling is essential to prevent warping and minimize cycle time. |
| Ejection System | Ejector Pins, Blades, Sleeves, Ejector Plates | Pushes the solidified part out of the B-side of the mold. | Ejector pins must be placed on strong, non-cosmetic areas to avoid marks. |
| Venting System | Vents (tiny gaps) | Allows air trapped in the cavity to escape as plastic flows in. | Poor venting can cause incomplete parts (short shots) or burn marks. |
Thinking about these systems while you design is the difference between a good part and a great, manufacturable part.
Why Injection Molding Can Be Economical at Repeated Volume
Injection molding converts a substantial design-and-tooling investment into repeated parts. Its economic value depends on accepted quantity, cavities, demonstrated cycle, uptime, yield, secondary work, inspection and maintenance. It is not proven by an unverified story or a universal percentage saving.
Compare alternatives at the same function and quality level: total route cost = fixed engineering/tooling + accepted quantity × variable cost per accepted part + logistics and lifecycle support. Machining or additive production may remain preferable for prototypes, uncertain demand or frequently changing geometry; molding becomes attractive when its repeatability and throughput offset the fixed investment.
Production readiness requires more than one good sample. Agree resin and machine, process record, cavity identification, dimensional/appearance/functional acceptance, correction closure, maintenance and handover. Use production injection molding for the part-supply scope and export mold manufacturing when the tool will run elsewhere.
What the Mold Contains
The core and cavity form the part, while the base supports and aligns them. Runners and gates deliver melt, vents release air, cooling removes heat, and ejectors or side actions release the finished geometry. Inserts and wear components protect areas that need service or frequent replacement.
How a Cycle Uses the Mold
The machine closes the mold, injects and packs resin, holds it while the gate freezes, cools the part, opens the tool and ejects or transfers the part. The mold must tolerate pressure, heat, movement, contamination and repeated cycles without losing alignment or surface.
Why Mold Design Changes Unit Cost
Cavity count, hot runner, slides, lifters, steel, polish, texture, cooling, inspection and spare parts influence tool price and production economics. A lower-cost mold can be the wrong choice if it creates high scrap, slow cycle or difficult maintenance.
What Makes a Mold Production-Ready
A production-ready tool has validated fill, dimensions, appearance, ejection, cavity balance, cycle, process window, maintenance access and documentation. One good sample is not enough evidence for a long production life.
Think of the Tool as a Lifecycle Asset
Cleaning, lubrication, cooling, wear inspection, spare inserts, repairs and revision control preserve performance. The mold’s value is measured over the parts it produces, not only when it leaves the mold shop.
What Exactly Is an Injection Mold? A Production-System Explanation: Buyer Review Checklist
- Review core, cavity, base, feed, venting, cooling, ejection, side actions and service features.
- Understand the complete fill, pack, cool, open and eject cycle.
- Compare cavity, hot runner, steel, surface, cooling, maintenance and spare requirements.
- Require trial evidence for dimensions, appearance, balance, cycle, ejection and process window.
- Plan maintenance, repair, documentation and ownership for the mold lifecycle.
FAQ
What is the difference between an injection mold and a mold base?
The mold base supports and aligns components; the complete injection mold also includes core, cavity, feed, cooling, ejection and any side actions that form the product.
How do I know an injection mold is ready for production?
Review repeat trial data for dimensions, appearance, balance, cycle, ejection, process window, inspection and maintenance documentation.
Conclusion
An injection mold is the coordinated tooling system that forms, supports, cools, vents, releases and ejects a part on a defined machine. Its value comes from an approved architecture, process window and lifecycle record—not from a steel label or the fact that the tool opens and closes.