
Are you relying on injection molding for every project? It’s a powerful tool, but assuming it’s generally the best choice can be a costly mistake. You might be missing out on faster, cheaper, or more suitable manufacturing methods. This uncertainty can lead to inefficient production and missed opportunities.
Injection molding is excellent for repeatable plastic production, but it is not necessarily the best first choice. A better process depends on volume, geometry, material, tolerance, launch timing, surface requirements and how much design uncertainty remains.
Related CKMOLD resources: injection mold services, DFM analysis, mold design, mold testing and validation, and production injection molding.
The best process depends entirely on your project’s specific needs. For high-volume, complex parts, injection molding is often unbeatable. However, for long, continuous profiles like pipes or window frames, extrusion is faster and more efficient. For low-volume prototypes or highly intricate custom parts, 3D printing offers superior design freedom and no tooling costs. For hollow items like bottles, blow molding is the standard. The “better” process is the one that aligns with your volume, budget, material, and design complexity.
Choosing a manufacturing process is one of the most critical decisions you’ll make. It impacts your budget, timeline, and the final quality of your product. While injection molding is my bread and butter, I’ve learned that being a true expert means knowing its limits and understanding the alternatives. Sticking to one method out of habit can hold your projects back.
What is better than injection molding?
You’re an expert in your field, but the constant stream of new and old manufacturing techniques can be overwhelming. It’s hard to know if you’re making the most optimal choice or just sticking with what’s familiar. This doubt can be frustrating when you’re trying to innovate and improve efficiency. I’m here to cut through the noise and give you a clear comparison of the main players in plastic manufacturing.
There is no single process that is universally “better” than injection molding. The ideal choice is relative to the application. For example, extrusion molding is superior for producing continuous linear shapes like tubing and seals due to its high speed and efficiency. Blow molding is the go-to for hollow parts like bottles and tanks. And for large, simple parts like trays or enclosures, thermoforming can offer lower tooling costs and faster setup times, making it a strong contender.
Use our broader alternatives to injection molding comparison when you need to screen machining, additive manufacturing, casting, forming and molding routes against the same project inputs.
Key Alternatives and Their Strengths
The best way to understand the alternatives is to see how they stack up against injection molding based on what you’re trying to achieve. Each process was developed to solve a specific manufacturing problem.
| Feature | Injection Molding | Extrusion | Blow Molding | Thermoforming |
|---|---|---|---|---|
| Part Geometry | Complex, 3D shapes | Continuous 2D profiles | Hollow 3D shapes | Simple, shallow 3D shapes |
| Best For | Housings, gears, caps | Pipes, seals, frames | Bottles, tanks, containers | Trays, packaging, covers |
| Tooling Cost | High | Low to Medium | Medium | Low to Medium |
| Production Speed | High (per part) | Very High (linear feet) | High | Medium to High |
| Wall Thickness | Precise control | Uniform | Less control | Can be uneven |
What is cheaper than injection molding?
The high upfront cost of an injection mold can be a major roadblock. You have a brilliant product idea, but the five or six-figure price tag for tooling stops you in your tracks, especially for a new product with unproven demand. This financial barrier can kill innovation and prevent great designs from ever reaching the market.
For low volumes, compare additive manufacturing, machining and appropriate forming/casting routes against the actual geometry and material. Tooling, fixtures, finishing, inspection and setup still affect total cost. There is no universal break-even volume or cheapest process for every prototype.
Breaking Down the Costs
The key to understanding which process is “cheaper” is to look at two things: the initial tooling cost and the per-part cost. Your total production volume determines which one matters more.
| Process | Tooling Cost | Per-Part Cost (Low Vol) | Per-Part Cost (High Vol) | Best for Volume |
|---|---|---|---|---|
| Injection Molding | Project-specific; request a scoped quotation. | Depends on geometry, material and operations. | Depends on cycle/build strategy and accepted yield. | Evaluate the actual demand and part requirements. |
| 3D Printing | Project-specific; request a scoped quotation. | Depends on geometry, material and operations. | Depends on cycle/build strategy and accepted yield. | Evaluate the actual demand and part requirements. |
| Vacuum Forming | Project-specific; request a scoped quotation. | Depends on geometry, material and operations. | Depends on cycle/build strategy and accepted yield. | Evaluate the actual demand and part requirements. |
| Rotational Molding | Project-specific; request a scoped quotation. | Depends on geometry, material and operations. | Depends on cycle/build strategy and accepted yield. | Evaluate the actual demand and part requirements. |
Calculating Your Break-Even Point
The “break-even point” is the production volume where the high tooling cost of injection molding becomes justified by its extremely low per-part cost.
- For prototypes and very low volumes: Additive manufacturing avoids a dedicated production mold, but compare it with machining and other routes. Material equivalence, build preparation, supports, finishing and inspection can change both cost and lead time.
- For intermediate quantities: Compare the same part specification, not a fixed volume band. Forming and rotational molding apply to different geometry envelopes and may need trimming or assembly; a process cannot win on tooling cost if it cannot make the required product.
- For stable repeat demand: Injection molding can distribute tooling cost across many parts, but the crossover depends on tool investment, accepted-part cost and design stability. High volume alone does not make it feasible for every geometry or eliminate the need to compare alternatives.
Is 3D printing better than injection molding?
You see headlines everywhere praising 3D printing as the future of manufacturing. There’s pressure to adopt it, and you wonder if it’s time to abandon traditional methods like injection molding. But you’re also skeptical. Can a 3D-printed part really match the quality and speed you need for a final product? This conflict can make it hard to decide which technology to invest your time and budget in. Let’s set the record straight.
3D printing is better than injection molding for rapid prototyping, creating highly complex or customized parts, and for very low-volume production runs. Its key advantage is the complete freedom of design without the need for expensive tooling. However, injection molding is far superior for mass production. It offers incredible speed, a very low cost per part at scale, better surface finishes, and a wider range of engineering-grade materials with more consistent mechanical properties. They are complementary tools, not direct competitors.
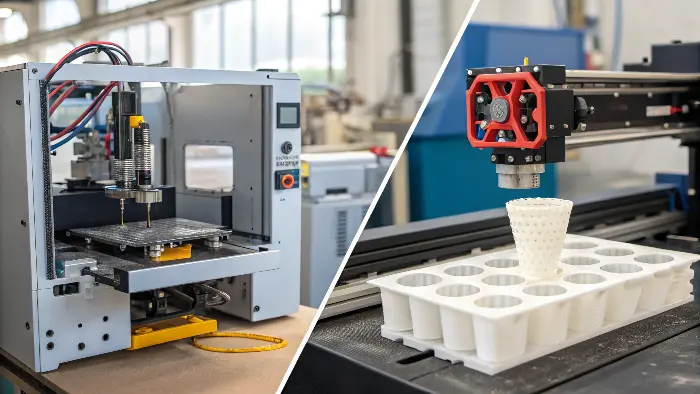
Illustrative development scenario—not a documented CKMOLD customer case: print an interlocking assembly before committing to a mold, then compare fit and accessibility. A prototype can reveal design problems, but its material, orientation and process may not reproduce molded fatigue, shrinkage or surface behavior. Confirm those separately before release.
A Head-to-Head Comparison
To really understand where each process shines, you need to compare them across the factors that matter most in product development and manufacturing.
| Feature | 3D Printing (Additive) | Injection Molding (Forming) |
|---|---|---|
| Speed (per part) | Slow (hours per part) | Fast (seconds per part) |
| Upfront Cost | None (for tooling) | Very High (for mold) |
| Cost per Part | High and relatively constant | Decreases dramatically with volume |
| Design Freedom | Nearly unlimited complexity | Limited by moldability (draft, undercuts) |
| Material Properties | Good, but can be anisotropic | Grade-, flow- and process-dependent; fibers and polymer orientation can create anisotropy. |
| Surface Finish | Often requires post-processing | Can be excellent, straight from mold |
| Best For | Prototypes, custom parts, low volume | Mass production, high-volume parts |
Speed and Scale: The Deciding Factor
Throughput must include batch size, parallel printers, nesting, setup, finishing and accepted yield. Injection molding adds mold-build and qualification time before repeat cycles. Compare end-to-end delivery for the required quantity; multiplying one printer cycle by quantity does not describe every additive-production plan.
Design Freedom vs. Design for Manufacturability
3D printing allows you to create geometries that are impossible to mold, like internal lattice structures or parts-within-parts. This is its superpower. Injection molding, however, requires you to follow strict “Design for Manufacturability” (DFM) rules. You need to think about draft angles so the part can be ejected, uniform wall thickness to prevent sink marks, and how to handle undercuts. While this seems restrictive, these principles often lead to a stronger, more efficient final part design.
What is the difference between RTM and injection molding?
You might hear the term Resin Transfer Molding (RTM) used for high-performance parts in the automotive or aerospace industries. On the surface, it sounds a lot like injection molding—you’re injecting a material into a mold. This similarity can be confusing. Choosing the wrong one because you misunderstand their fundamental differences could lead to a product that is too heavy, too weak, or far too expensive for its application. Let’s clarify exactly what sets them apart.
The primary difference is the material and the process sequence. Injection molding injects molten thermoplastic into an empty mold cavity. Resin Transfer Molding (RTM) first places a dry fiber preform (like carbon or glass fiber) into the mold, closes it, and then injects a liquid thermosetting resin. This resin saturates the fibers and cures, creating a high-strength, lightweight fiber-reinforced composite part. Injection molding makes plastic parts; RTM makes composite parts.
Illustrative process-selection scenario: a high-stiffness bracket may justify continuous-fiber RTM when a short-fiber injection-molded option cannot meet the load case. Compare laminate design, inserts, testing, tooling and cycle together. No specific weight saving or customer outcome is established by this example.
Core Process and Material Distinctions
Understanding the “how” and “what” of each process reveals why they are used for such different applications. They are fundamentally different approaches to creating a final shape.
| Feature | Injection Molding | Resin Transfer Molding (RTM) |
|---|---|---|
| Material Type | Thermoplastics (PE, PP, ABS, PC) | Thermosetting Resins (Epoxy, Polyester) |
| Reinforcement | Optional (short fibers mixed in) | Required (long fiber preform) |
| Process | Inject melted plastic into empty mold | Inject liquid resin into mold with fiber |
| Part Strength | Good to Very Good | Exceptional (high strength-to-weight) |
| Cycle Time | Fast (seconds to minutes) | Slow (minutes to hours) |
| Tooling Pressure | Very High | Low to Medium |
| Typical Apps | Consumer goods, enclosures, gears | Aerospace structures, race car bodies |
The Role of Reinforcement in RTM
The star of the RTM show is the fiber preform. This isn’t just a handful of short fibers mixed into the plastic like you might find in glass-filled nylon. This is a strategically designed fabric or mat of continuous fibers (like carbon, glass, or aramid) that forms the structural backbone of the part. The resin’s job is simply to hold these powerful fibers in place. This is why RTM parts can achieve strength properties similar to metals but at a fraction of the weight. In injection molding, the plastic itself provides the bulk of the structure.
Pressure and Tooling Considerations
Thermoplastic injection tooling may use aluminum, prehardened or through-hardened steel according to duty and program needs. RTM tooling also varies with pressure, temperature, size and life. Pressure differences do not create one mandatory tooling material or a universal cost advantage.
When CNC Machining or 3D Printing Makes More Sense
CNC machining is useful for prototypes, tight-machined features or low-volume parts where tooling cost is not justified. 3D printing is useful for design iteration and complex shapes, but material properties and surface finish may not match molded parts. These processes can reduce early risk before mold investment.
When Injection Molding Becomes the Better Route
Once volume increases and the design stabilizes, injection molding usually offers better unit cost, repeatability and material options. It also supports integrated features such as bosses, clips, ribs and textures. The key is not to start tooling before the design is ready.
Hybrid Development Plans Often Work Best
Many projects use 3D printing or CNC first, then prototype tooling, then production tooling. CKMOLD can help customers compare routes based on total project risk rather than one-part price. The best route is the one that gets a manufacturable part to market with the least avoidable rework.
When Is Another Process Better Than Injection Molding: Buyer Review Checklist
- Use 3D printing for fast form and fit learning when material equivalence is not critical.
- Use CNC for low-volume precision prototypes or machined material validation.
- Use prototype tooling when molded material behavior must be tested.
- Use production molding when volume and design stability justify the mold investment.
- Compare total cost, timing and risk instead of only unit price.
FAQ
Is 3D printing better than injection molding?
It can be better for fast prototypes and design changes, but injection molding is usually better for repeatable production with molded-grade materials.
When should I move from CNC to injection molding?
Move when the design is stable, expected volume is high enough and molded material/process behavior needs to be validated.
Compare Routes Using the Same Delivered-Part Specification
Define geometry, material function, final finish, tolerance, accepted quantity and delivery date before comparing processes. A printed appearance model and a molded production component do not answer the same purchasing question. List additional supports, trimming, joining, coatings, fixtures and qualification needed to reach the delivered condition.
For a simplified two-route screen, total cost is fixed setup/tooling plus quantity multiplied by accepted-part cost. The crossover is the fixed-cost difference divided by the variable-cost difference, only when the latter favors the higher-investment route. If capacity, yield or design revisions differ, compare scenarios rather than presenting one universal quantity threshold.
Protolabs’ additive-to-molding discussion is useful for planning the transition. The CNC DFM guide covers machined geometry; the plastic moulding overview defines the process families. For an injection-molding feasibility enquiry, state which prototype requirements remain unproven and when production demand becomes firm.
If ABS injection molding is selected, use the measured waste-and-energy review to evaluate improvement within that route rather than relying on a green label.
Conclusion
Injection molding is an incredibly powerful and efficient manufacturing process, but it’s not the only tool in the shed. The “better” process doesn’t exist in a vacuum; it is generally the one that best fits your specific project goals. By understanding the unique strengths of alternatives like extrusion, 3D printing, and RTM, you can make smarter, more effective decisions. Choosing the right process is the first step to mastering your craft and bringing successful products to life.