
Automotive interior appearance depends on the complete surface system: steel preparation, texture or polish, gate and venting, resin/color, process, geometry, assembly and the viewing standard. Polishing alone cannot remove a flow, sink, weld or grain-matching problem.
For each visible zone, define the required grain or polish, gloss/color master, allowable defects, touch points and repair boundary. Select steel and finishing methods from the exact texture, resin, volume and maintenance plan; then approve representative molded parts.
A buyer should separate three questions: what the steel surface is, what the molded part looks and feels like, and how the appearance will be held through maintenance. Each needs its own controlled reference and inspection record.
Automotive interior surfaces are judged under controlled lighting, close viewing and repeated handling, so a small mismatch, gloss shift or texture defect can become a customer-visible issue. Mold polishing for interior components must coordinate steel preparation, texture or gloss specification, parting lines, gate strategy, release, inspection and molded-sample approval.
Related CKMOLD resources: mold design services, mold testing and validation, production injection molding.
Why is consistent Surface Finish So Critical for Automotive Interior Appeal and Functionality?
Seeing minor flaws in a new car’s trim? It’s disappointing, right? These small defects can disproportionately impact the perceived value and quality of the entire vehicle, affecting customer satisfaction and brand reputation. It’s a real headache.
A consistent surface finish is critical for automotive interiors because it directly influences customer perception of quality, enhances tactile experience, and ensures components fit reliably. It’s not just about looks; it’s about the brand’s promise of excellence.
Think about the first time you sit in a new car. What do you notice? Often, it’s the details – the way the light catches the dashboard, the feel of the center console, the precision of the knobs and buttons. I’ve had countless conversations with automotive designers and engineers, and they all stress the same thing: the interior sells the car as much as the exterior or performance these days.
The “Touch and Feel” Factor
Automotive interiors are highly tactile environments. Drivers and passengers are constantly interacting with surfaces. A cheap-feeling, poorly finished component can make an otherwise great car feel, well, less than premium. A smooth, blemish-free surface, or a reliably rendered texture, communicates quality and care. For example, a high-gloss “piano black” finish on a center console needs to be absolutely suitable – any swirl mark or pinhole stands out like a sore thumb. Similarly, a grained texture on a door panel needs to feel consistent and authentic.
Brand Perception and Quality Cues
Preventing Assembly Issues and Rattles
Beyond aesthetics, surface finish can also impact functionality. Poorly finished mold surfaces can lead to parts with slight dimensional inaccuracies or flash. These might not seem like big deals, but in a complex assembly like a car interior, they can cause fitment issues, leading to squeaks, rattles, or unsightly gaps. For the buyer, ensuring his components integrate seamlessly is vital for his customers, the automotive OEMs. A good polish helps ensure parts come out of the mold exactly as designed.
What Specific Polishing Techniques Do We Employ for Diverse Automotive Interior Textures?
Automotive interiors feature diverse textures, from high gloss to subtle grains. Achieving each reliably requires more than a one-size-fits-all polish. Incorrect techniques mean parts that don’t match or feel cheap, a real nightmare for any supplier.
We employ specific, multi-stage polishing techniques tailored to each required automotive interior texture, from mirror-like SPI A1 for chrome-look accents to precise VDI or custom graining for tactile surfaces. This ensures consistent and accurate texture replication on every part.
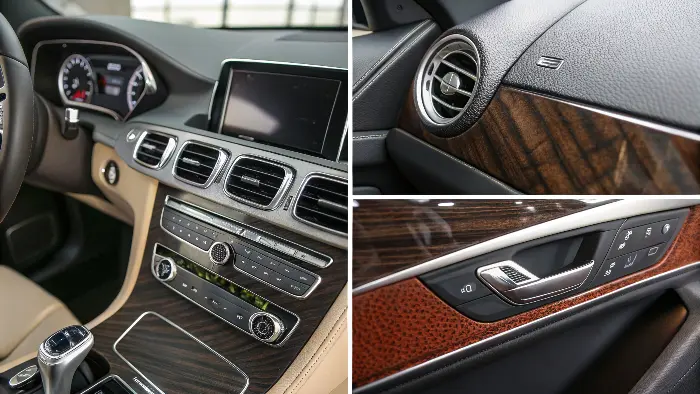
The variety in automotive interiors is amazing, isn’t it? You’ve got super shiny bits, parts that look like brushed aluminum, soft-touch surfaces, and all sorts of grained patterns. Each of these needs a different approach when it comes to polishing the mold. It’s not just about making it smooth; sometimes it’s about preserving or even enhancing a texture.
High-Gloss Finishes (e.g., Piano Black, Chrome-look)
Textured Finishes (e.g., Leather Grain, Technical Grains)
Many automotive parts have textures – leather grain on dashboards, technical patterns on door inserts, or even custom-designed grains. Often, these textures are applied to the mold via chemical etching or laser texturing. The polishing work around these textured areas is critical. Before texturing, the surface needs to be polished to a specific VDI (German standard) or SPI C/B level to ensure the texture takes evenly. After texturing, any surrounding areas that need to be glossy must be polished without damaging the delicate texture. This requires incredible skill and often custom-made soft tools.
Matte and Satin Finishes
| Not everything is shiny. Some parts require a matte or satin finish – think of certain buttons, control panels, or low-glare surfaces on the dashboard. These are typically achieved with very fine abrasive blasting (like bead blasting) or sometimes by a very fine paper or stone finish (like an SPI C-1 or D-1). The trick here is uniformity. Any unevenness in the blast or polish will be obvious on the final part. Here’s a quick look at how we approach common automotive needs: |
Interior Component Example | Desired Finish | CKMOLD Polishing Focus |
|---|---|---|---|
| Center Console Trim | Piano Black (High Gloss) | SPI A1, multi-stage diamond, pristine steel (e.g., S136) | |
| Dashboard Top | Leather Grain Texture | Prepare for VDI/etching, protect texture, consistent matte | |
| Air Vent Louvers | Satin Finish | Uniform fine paper/stone or controlled blast, edge precision | |
| Door Panel Inserts | Technical Grain | Careful prep for texture, polishing adjacent smooth areas | |
| Control Knobs/Buttons | High Gloss with Matte | Combination polishing, masking, extreme precision |
It’s this attention to detail for each specific need that sets a quality molder apart.
How Should Large, Curved and Deep Automotive Mold Surfaces Be Controlled?
Large visible surfaces, fine details and deep features fail in different ways, so they should not be covered by one claim of polishing skill. Divide the tool into controlled zones and preserve datums, form, shutoffs, edge radii and texture boundaries while the surface is prepared.
| Surface zone | Main risk | Control and acceptance evidence |
|---|---|---|
| large or gently curved A-surface | waviness, gloss bands, local over-polish | controlled support/tool path, form check and molded appearance under defined lighting |
| small details, vents and sharp transitions | rounded edges, changed gaps or lost texture boundary | protected edges, shaped laps/tools, dimensional check and approved molded transition |
| deep ribs or restricted access | uneven stock removal, trapped abrasive and damaged rib walls | access-specific tool, cleaning, draft/release review and repeated ejection evidence |
Where a zone cannot be seen or measured reliably during hand work, agree the intermediate inspection method and stop criterion before polishing. A supplier should show how the final mold geometry and the molded appearance or release result are both verified.
How Does Steel Selection Affect Automotive Surface Work?
Polishability and texture response depend on the exact producer grade, cleanliness, hardness, heat treatment, machining/EDM history, weld repairs and section size. P20-family, NAK80-family and stainless mold-steel names are not universal finish grades and are not automatically equivalent across producers.
Uddeholm’s polishing guidance describes how steel quality, heat treatment, machining condition, abrasive sequence, cleanliness and pressure affect the result. Daido’s NAK80 product information describes that specific prehardened grade; Uddeholm’s Stavax ESR heat-treatment data applies to that named grade. Use these as grade-specific examples, not as permission to substitute one designation for another.
| Buyer question | Supplier evidence |
|---|---|
| Which steel forms each visible zone? | producer, exact grade, supply condition and component-level steel map |
| How is the target surface produced? | machining/EDM condition, heat treatment, texture/polish specification and sequence |
| How will repairs be controlled? | weld/repair limits, blend area, retexture/repolish method and reapproval rule |
| How is uniformity accepted? | molded master, viewing conditions, gloss/color/texture zones and defect boundary |
How Should Finish Consistency Be Controlled Over Tool Life?
Automotive appearance is approved on a molded surface under defined viewing conditions—not by stating that an internal SOP exists. Record the steel condition, abrasive or texture process, direction, protected edges, approved master, process window and inspection method. Different technicians should work from the same controlled record.
The DME micro-finish guide ties A, B, C and D reference finishes to stated preparation media and reports approximate Ra for those conditions. It is a mold-steel reference, not a universal molded-part roughness or gloss guarantee.
Maintenance should trigger inspection from actual wear, gloss/texture drift, deposits, venting or repair—not a promise that polish itself prevents wear. After local steel repair or repolishing, recheck the molded transition under the approved appearance conditions and update the tool history.
Define the Visible Zone and Reference Standard
Identify Class-A or customer-visible areas, reflection direction, grain or texture, gloss range, acceptable flow marks and match requirements between adjacent components. A surface can be dimensionally correct and still fail because its texture or reflectivity does not match the reference.
Protect Grain and Texture During Steel Work
Texture-ready surfaces need the correct steel condition, machining allowance and edge definition. Polishing may be required before texturing, but excessive work afterward can alter grain depth or direction. Corners, shutoffs and transitions need special review because texture continuity is difficult to recover after damage.
Control Parting Lines, Gates and Weld Lines
Visible interfaces should be positioned and finished deliberately. Gate marks, weld lines and trapped gas can create appearance defects that no amount of polish will remove. Flow analysis, gate review and venting are part of the surface solution.
Validate Scratch, Gloss and Handling Resistance
Interior parts may be wiped, touched, assembled and exposed to heat or cleaning agents. Molding trials should assess gloss, grain, scratch or scuff behavior, fit, color and the effect of handling. Use consistent lighting and sample conditioning for decisions.
Document the Finish for Future Maintenance
Record texture or gloss standard, steel area, polish sequence, reference samples, inspection method, repair restrictions and approved process. If a cavity is polished or repaired later, the team needs a clear baseline to restore the appearance rather than create a new one.
Automotive Interior Mold Polishing: Buyer Review Checklist
- Define visible zones, grain or texture, gloss, lighting and customer reference before tooling.
- Protect steel condition, edges, shutoffs and texture continuity during polishing and texturing.
- Coordinate gate, venting, flow and parting-line choices with appearance requirements.
- Validate molded appearance, scratch, scuff, handling, fit and environmental exposure.
- Document the finish standard and repair limits for future mold maintenance.
FAQ
Why can adjacent automotive interior parts look different?
Texture, gloss, color, resin lot, mold temperature, flow direction, polishing or viewing condition can create differences even when the CAD shape is similar.
Can a damaged texture be repaired by polishing?
Sometimes the area must be re-prepared and re-textured; polishing alone may change the grain or create a mismatch.
Conclusion
Automotive interior finish is a repeatable approval system, not simply a high-gloss polish. Define visible zones and masters, choose exact steel and surface processes, control flow and part interfaces, approve representative molded parts and preserve the repair/maintenance history.