
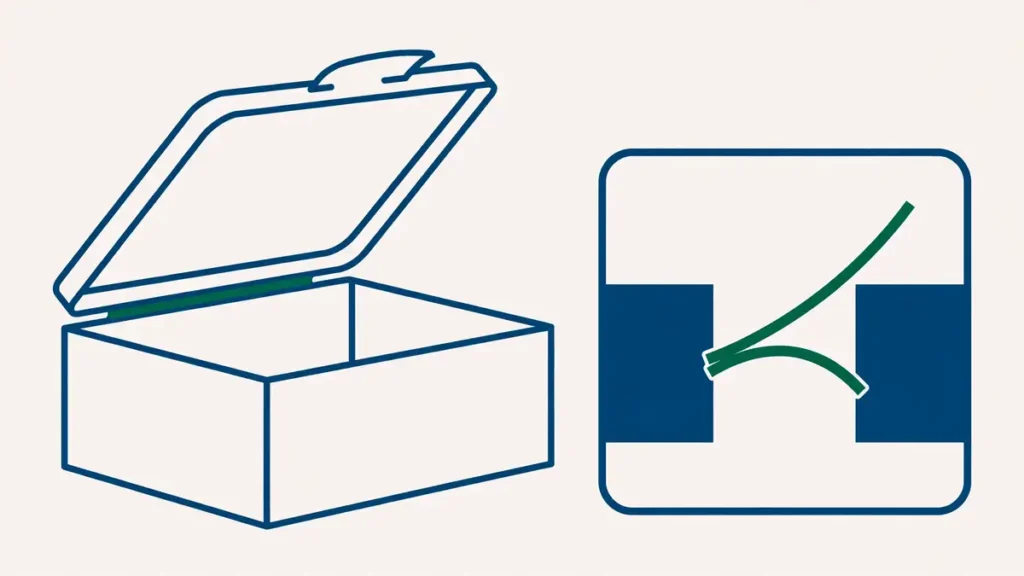
A flip-top cap opens fine on the first ten tries, then a white line appears across the hinge, and by the hundredth opening it snaps. The buyer blames the material. The molder blames the design. Both are half right, and neither half fixes the part on its own. A living hinge that survives is decided by three things together: the ratio of hinge thickness to hinge width, the grade of polypropylene, and the direction the melt flows across the hinge. Get all three right and a well-made polypropylene hinge can outlast the product it belongs to. Get any one wrong and no resin change will save it.
A living hinge is a thin, flexible web of plastic molded as part of the component itself, connecting two thicker wall sections so they can fold against each other without a separate hinge, pin, or fastener. It is the reason a shampoo cap, a wet-wipe lid, a toolbox, or a small-parts storage box can be molded as one piece instead of two parts plus an assembly step. That single-piece construction is the whole business case: fewer components, no hinge hardware, no assembly labor. But it only pays off if the hinge keeps flexing for the life of the product. This guide explains how to judge whether a hinge design will last, how to check the numbers on your own drawing, and what to put in an RFQ so a supplier can quote the hinge rather than guess at it.
When a Living Hinge Is the Right Answer — and When It Is Not
The first decision is not a dimension. It is whether a living hinge belongs on the part at all. A living hinge is a fatigue component: every opening bends the same thin section, and the material either survives that bending or it does not. It works best where the hinge is short, the opening angle is up to about 180 degrees, the load is light, and the part will be opened and closed many times over a long service life. Caps, lids, closures, small cases, and dispenser covers are the classic applications. A hinge that only needs to fold once during assembly, or that carries a heavy lid, or that must hold a precise angle under load, is a different problem.
| What the part needs | Best route | Why |
|---|---|---|
| Lid opened and closed daily for months or years | Living hinge in polypropylene | No hardware, no assembly, proven fatigue life in the right geometry |
| Lid folded once at assembly, then stays shut | Living hinge, or a snap-fit lid | Hinge life is not the constraint; choose on tooling cost |
| Heavy lid, or hinge must hold an angle under load | Separate pin hinge or metal hinge | A thin plastic web cannot carry that load or hold that position |
| Hinge longer than about 150 mm (6 in) | Split the hinge into two or more sections with gaps | Long single hinges flex unevenly and stress the tool; segmented hinges last longer |
| Part in a stiff resin (ABS, PC, nylon) with no material freedom | Separate hinge or redesign in PP/PE | Stiff resins fatigue-crack after limited flexes; the hinge will fail first |
| Transparent lid with a hinge | Living hinge in a clear-tough resin, with a flex test | Clear resins are stiffer and weaker in fatigue; test before committing |
If the part is large, the honest answer is usually that a living hinge will not work. The molecules of molded polypropylene only orient themselves properly in narrow sections, so a very thick hinge on a large part cannot develop the oriented structure that gives a hinge its fatigue life. A supplier who tells you a living hinge is unsuitable for a large, heavy lid is not being unhelpful; they are saving you a failed tool.
The Three Numbers That Decide Hinge Life
Once a living hinge is the right route, three dimensions do most of the work: hinge thickness, hinge land length, and the radius on the outside of the bend. The published guidelines from different sources agree closely, which is reassuring: this is settled engineering, not fashion.
| Dimension | Starting point (polypropylene) | What happens if you get it wrong |
|---|---|---|
| Hinge thickness | 0.20–0.38 mm (0.008–0.015 in); start thin at 0.20–0.25 mm and adjust up | Too thick: the outer fibers stretch past the material’s limit every time it bends, and it cracks. Too thin (below 0.20 mm): excessive pressure drop, shear heat, short shots, or an underpacked hinge |
| Hinge land length (the thin section) | About 1.5 mm (0.060 in) | Too short: the bend concentrates in one line and the hinge is over-stressed. Too long: high pressure drop across the hinge, underpacking, and a loose-fitting lid |
| Outside bend radius | About 0.75 mm (0.030 in), with generous radii on both transitions | Sharp corners act as stress risers; the crack starts exactly there |
| Recess on the folding side | 0.13–0.25 mm (0.005–0.010 in) | Without a recess, the hinge folds sharply on itself when closed and the mating parts do not sit properly |
Protolabs’ published starting point is 0.012 in (0.30 mm) thickness with 0.060 in (1.5 mm) spacing, a 0.008 in reduction on the side the part folds toward, and a 0.030 in radius on the opposite side, where most of the tensile strain occurs. Dow’s Robert Cramer, writing in Plastics Today, gives the same proportions: a land of 0.060 in (1.5 mm), thickness 0.008–0.015 in (0.20–0.40 mm), radii of 0.030 in (0.75 mm), and a recess of 0.005–0.010 in on the upper surface. MIT’s living hinge design notes add the steel-safe rule that matters most to a buyer paying for a tool: start with a thin hinge, 0.008–0.010 in (0.20–0.25 mm), and adjust upward if needed, to a maximum of 0.015 in (0.38 mm). Starting thin is steel-safe because steel can be removed from the mold to thicken a hinge, while thickening a hinge that started too thick requires welding the mold and recutting — slower and more expensive.
The thickness number deserves a second look, because it runs against intuition. A thicker hinge looks stronger. In a living hinge it is weaker. Bending a thick section stretches the outer fibers much further than bending a thin one, so the surface of a thick hinge exceeds the material’s ultimate elongation and cracks, while a thin hinge of the same material bends elastically. This is the single most common design error in living hinges, and it is also the easiest to check on a drawing: if the hinge on your part is 0.6 mm thick, it is almost certainly too thick, whatever the rest of the design looks like.
There is one more geometric detail worth checking. Where a hinge meets a snap-on latch or a lid that twists as it opens, the maximum stress develops at the two ends of the hinge, and tears start there. MIT’s notes describe three defenses: thicken the hinge slightly at both ends (for example from 0.25 mm to 0.50 mm over a 0.5–1.0 mm length, then blend back), add a 0.13 mm film at both ends parallel to the hinge plane, or radius the hinge ends. The thin film at the ends is reported to increase the torque-to-failure ratio tenfold once it is flexed the first time and becomes highly oriented. If your hinge tears at the ends rather than across the middle, this is the fix to ask for.
A Worked Check: the Thickness-to-Width Ratio
Guidelines are useful, but a buyer with a drawing in hand wants a check, not a slogan. There is a published method for one, developed by Dow’s Robert Cramer and described in Plastics Today. The critical parameter is the ratio of hinge thickness to hinge width — call it b/L, where b is the hinge thickness and L is the land length. The smaller the ratio, the less likely the hinge is to fail. For the typical proportions above, the ratio falls between 0.13 and 0.25. If your drawing’s ratio sits well above that band, the hinge is at risk before a single part is molded.
Work through it with a flip-top cap hinge, using numbers a buyer can measure on a drawing:
- Hinge thickness b = 0.30 mm, land length L = 1.5 mm.
- b/L = 0.30 / 1.5 = 0.20. That sits inside the typical 0.13–0.25 band. The proportions are consistent with a durable hinge, provided the material and the gate placement are also right.
- Now suppose someone "strengthens" the hinge by thickening it to 0.50 mm, keeping the same 1.5 mm land. b/L = 0.50 / 1.5 = 0.33. That is outside the band, and the hinge is now more likely to crack, not less — the thicker section stretches its outer fibers further on every bend.
- To fix a 0.50 mm hinge without touching the tool steel for the hinge thickness, widen the land instead: at L = 2.5 mm, b/L = 0.50 / 2.5 = 0.20, back inside the band.
That last move — widen the land instead of thinning the hinge — is exactly how a real failure was fixed. Cramer describes a manufacturer of storage boxes for small fasteners who molded a lid and box body as one part in polypropylene. The hinge cracked after only a few cycles. The resin had a yield stress of 34.5 MPa, a modulus of 1,379 MPa, and an ultimate elongation of 100%. The original hinge was 0.60 mm thick and 1.5 mm wide: b/L = 0.40, far above the typical band, and the analysis showed the bending and tension exceeded the material’s ultimate elongation. Two fixes were considered. Reducing the thickness to 0.50 mm would have worked on paper, but it would have required welding the mold and recutting the hinge area. Widening the hinge to 2.0 mm instead gave b/L = 0.30, kept the stresses within the material’s limits, required no welding, and the sample parts showed excellent fatigue life.
Treat this check as a screening tool, not a guarantee. It uses the published method and published material data, and it tells you whether the proportions are in the safe band or outside it. It does not replace a T1 sample and a flex test on real parts. But it does something a guideline alone cannot: it lets you look at a supplier’s drawing, run two numbers, and ask a precise question — "this hinge is at b/L 0.40, outside the published band; how are we bringing it back inside?" — before steel is cut.
Material: Why Polypropylene Wins, and Which Polypropylene
No geometry rescues the wrong resin. A living hinge needs a material that can be bent thousands of times without cracking, and very few plastics qualify. Polypropylene is the standard because its molecules orient along the flow direction when the melt is forced through the thin hinge section, and that orientation gives the hinge its fatigue strength. Polyethylene works too, but it usually does not match polypropylene’s hinge life, so it suits parts that are opened less often.
| Resin | Hinge life | When to use it |
|---|---|---|
| Polypropylene homopolymer | Best; a well-designed, well-molded hinge can survive hundreds of thousands to around a million flexes in published tests | The default choice for any living hinge |
| Polypropylene random copolymer | Very good, slightly below homopolymer | When you need a little more clarity or low-temperature toughness than homopolymer gives |
| Polypropylene impact copolymer | Weakest of the PP family for hinges | Only when cold-temperature impact resistance matters more than hinge life |
| Polyethylene (HDPE) | Good, but shorter hinge life than PP | Parts opened infrequently, or where PE’s other properties decide the material |
| K-Resin (styrene-butadiene) | Limited; usable with precautions | When a harder or clear material is required; flex the hinge while it is still warm off the press |
| ABS, PC, nylon, PET | Poor for repeated flexing | Avoid for living hinges; use a separate hinge or redesign in PP/PE |
Three material details matter more than the resin family name. First, the grade: homopolymer PP gives the best hinges because of its higher starting tensile strength and low tendency to whiten under stress; random copolymer is second; impact copolymer is the least desirable for hinges unless cold-temperature impact is a hard requirement. Second, melt flow rate: lower MFR means higher molecular weight, and higher molecular weight is better for hinge life — but lower-MFR resins are harder to mold through a thin hinge, so the grade is a balance the supplier should confirm against the part size. Third, fillers: talc, mica, and glass fiber compounded into polypropylene reduce elongation and can give very poor hinge life, so a filled grade chosen for stiffness elsewhere in the part can quietly kill the hinge. If the part needs a filled resin for structural reasons, say so in the RFQ and ask how the hinge will be protected — sometimes the answer is a different resin for the whole part, sometimes a design change.
How long should a hinge last? The honest answer is that it depends on the geometry, the grade, and the molding conditions, and any supplier who quotes a cycle count without those details is guessing. But published testing gives a sense of what a good hinge can do. MIT’s design notes record a homopolymer PP hinge (4 melt flow rate) flexed over a 180-degree angle 300,000 times at 23°C, then 300,000 times at −28°C, then 300,000 times at 23°C again — 900,000 flexes in total — without failure. Protolabs’ guide puts it more simply: a well-designed living hinge can last for up to a million cycles. Use those figures as a benchmark for what "good" looks like, not as a promise for your part. The cycle count that matters is the one you agree with your supplier and test on real parts.
Two environmental warnings from the same MIT notes are worth passing on. A living hinge does not stress-crack unless it is chemically attacked, but severe oxidizing environments and direct sunlight degrade polypropylene’s service life, and the thin hinge web is the most exposed part of the component. If the part will live outdoors or in contact with aggressive chemicals, the resin needs to be stabilized for that environment and tested for it — do not assume a standard grade will do.
Gate Placement and Flow: the Invisible Half of Hinge Design
A hinge can have perfect dimensions and the right resin and still fail, because how the melt flows across the hinge decides how the molecules orient — and orientation is what gives the hinge its strength. The rule is simple to state and easy to get wrong: the melt must flow perpendicular to the hinge, reach the entire width of the hinge as uniformly as possible, and keep flowing across it without hesitation.
In practice that means the gate is placed so the flow front hits the hinge evenly across its full width. If the melt reaches one end of the hinge first and hesitates at the rest, the hinge cools unevenly, a weld line can form along the hinge, and the hinge is weak from the first flex. For a long, narrow box and lid molded as one piece, a single center gate is a common mistake: the flow hits the hinge restriction before the gated cavity has filled, stops at the hinge while the rest of the cavity fills, and by the time pressure rises enough to push across, the hinge area has started to freeze — so melt flows across from both ends and meets in a weld line along the hinge, possibly with trapped air. The usual fixes are multiple gates or a long flash gate, or breaking a long hinge into two smaller segments with a gap in the middle, one gate opposite each segment.
Cooling matters as much as gating. The shear rate through a thin hinge is high during filling, which generates extra frictional heat, so the tool needs cooling channels running parallel and as close as possible to both sides of the hinge to remove that heat and preserve the molecular orientation set up during filling. Poor cooling in the hinge area is one of the quieter causes of weak hinges: nothing looks wrong on the drawing, and the parts fail anyway.
Two process details complete the picture. First, fill the part at a medium-to-high injection rate without step changes in the velocity profile; filling too slowly causes flow hesitation, which can lead to hinge delamination, and too low a melt temperature causes similar problems. Second, flex the hinge a few times immediately after molding, while the part is still warm. This first flexing — cold drawing — stretches the hinge web beyond its yield point without breaking it, orients the material in the right direction, and increases fatigue life. Protolabs makes the same point for harder resins: bend the hinge as it comes off the press while it is warm, which reduces tensile stress and the risk of cracking. If your supplier’s process does not include that first flexing, ask why.
When you review a supplier’s DFM report, the hinge is one of the things to look for in the gate and flow section: where the gates sit relative to the hinge, whether the flow reaches the hinge uniformly, and whether the report flags a weld line or hesitation at the hinge. Our guide to reviewing a DFM report before approving an injection mold walks through that review step by step, and the gate discussion there applies directly to hinges. Gate placement is also where a tolerance review earns its keep: a hinge thickness of 0.30 mm with a loose tolerance is a different part from the same hinge held tightly, and the drawing should say which one you are buying.
When a Hinge Fails: Reading the Failure
A failed hinge is a diagnostic instrument. Where and how it fails tells you what to fix, and the fix is rarely "use a stronger material."
| What you see | Most likely cause | What to change |
|---|---|---|
| Cracks on the first few flexes | Hinge too thick (b/L above the typical band), or a weld line across the hinge | Check the b/L ratio; widen the land or thin the hinge; move the gate so flow crosses the hinge evenly |
| White stress marks along the hinge | Bending strain above the resin’s allowable range; sharp corners | Increase the bend radius; lengthen the land; check the recess on the folding side |
| Hinge tears at the ends, not the middle | Twisting load at the hinge ends, common with snap-on latches | Thicken the hinge slightly at both ends, radius the ends, or add a thin film at the ends |
| Hinge lasts weeks, then cracks in service | Wrong resin grade or filler, UV or chemical attack, or no cold drawing after molding | Switch to homopolymer PP without fillers; stabilize the resin for the environment; flex hinges while warm |
| Hinge delaminates or splits along its length | Flow hesitation at the hinge, cold melt, or poor venting | Raise the fill rate smoothly, check melt temperature, verify vents and cooling at the hinge |
| Lid does not close flat, or the hinge folds sharply | No recess on the folding side, or land too short | Add the 0.13–0.25 mm recess; lengthen the land |
Notice what is missing from that table: "the material was bad." Resin quality matters, but most hinge failures trace back to proportions, flow, or a grade choice that was never matched to the hinge. That is good news for a buyer, because proportions and gate placement are visible on a drawing and a DFM report before any steel is cut. If a hinge is failing on a part that is already in production, the same table is the fastest route to a fix that does not require a new tool: widening a land, for example, can sometimes be done without welding, as the storage-box case above showed.
What to Put in the RFQ So the Supplier Can Quote the Hinge
A hinge fails most often before the RFQ is even written, when the drawing shows a thin section with no dimensions, no material grade, and no expectation of how many times it must open. A supplier cannot quote what is not specified, so the hinge gets whatever the default is — and the default is rarely your requirement. Send this with the RFQ:
- A drawing with the hinge section dimensioned: thickness, land length, bend radius, and recess, not just a thin line on a general view.
- The resin, by grade family: homopolymer PP preferred, with the melt flow rate if you know it, and a note if any filler is required elsewhere in the part.
- The expected hinge life, stated as a number and a test: for example, "50,000 open-close cycles at room temperature, 180-degree opening, tested on first-article parts." If you do not know the number, say how the product will be used and ask the supplier to propose one.
- The opening angle and the operating temperature range, including cold conditions if the product will see them.
- The part’s use environment: outdoor, UV exposure, contact with cleaners or chemicals.
- A request that the DFM report address the hinge specifically: gate position relative to the hinge, predicted weld lines, and the fill pattern across the hinge width.
- Whether the hinge will be flexed while warm after molding, and who is responsible for that step.
Send the 3D model and the 2D drawing together — the hinge dimensions belong on the 2D drawing, where a reviewer will actually see them. And if the part is a cap or closure, say so early: cap molds have their own hinge, thread, and sealing considerations, and our guide to plastic cap mold design covers the features that sit next to the hinge. The material comparison in our PP vs HDPE guide for containers and caps is also worth a read before you lock the resin, since the same grade decision affects both the hinge and the container body.
A living hinge is a small feature with an outsized effect on whether a product feels well made. Get the proportions inside the published band, choose a homopolymer polypropylene without fillers, gate the part so the melt crosses the hinge evenly, and flex it while it is still warm. Then test the first articles the way the product will actually be used — open and close them, in the cold if the product will see cold, until the agreed cycle count is reached. If the hinge survives that, the tool is doing its job. If it does not, the failure will tell you which of the three decisions to revisit.
If you are working on a part with a living hinge and want a second opinion on the drawing before you commit to tooling, send the 3D model, the 2D drawing with the hinge section dimensioned, the resin grade, and the expected cycle count through our request-a-quote page. We will review the hinge proportions, the gate position, and the material choice, and tell you what we would change before steel is cut.