
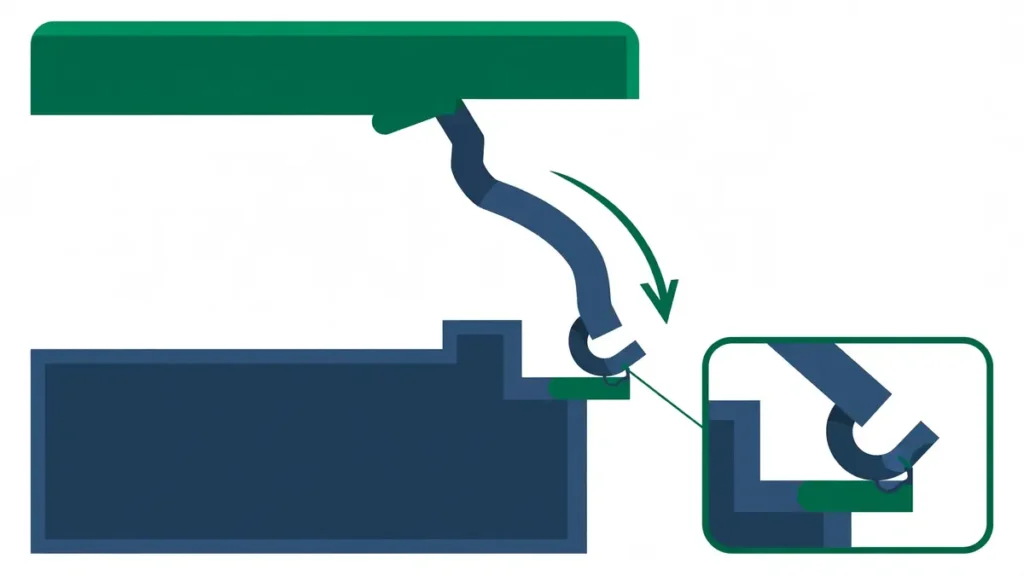
A housing lid that will not stay shut. A clip that cracks the first time a worker presses it home. A cover that assembles beautifully in the prototype and then pops open in the customer’s hands. Snap fits fail in exactly these ways, and almost every failure has the same root cause: nobody checked how far the material was asked to bend.
A snap fit is a strain problem before it is a geometry problem. Before you approve a design, check the peak strain at the arm root with ε = 1.5 × y × h ÷ L², and compare it with the resin’s allowable strain for a single assembly — 4% for unfilled polycarbonate, 2.5% for PC/ABS, according to Covestro’s design guide. If the check passes with margin, the clip will almost certainly survive; if it fails, no amount of tweaking the hook shape will save it.
This guide works from the failure backwards: what breaks, which joint type fits your part, the one calculation that decides the outcome, the forces your assembler will actually feel, what the clip costs in the mold, and what evidence to ask for before production.
Why do snap fits fail? Six failure modes and their fixes
Most snap-fit trouble shows up as one of six symptoms. Each points to a different decision made upstream — geometry, material, or mold design — and each has a fix that does not require starting the part over.
| Symptom | Most likely cause | Fix to try first |
|---|---|---|
| Clip cracks at the root on first assembly | Root strain exceeds the material’s allowable strain | Lengthen the arm, thin the root, or taper the arm; re-run the strain check below |
| Clip assembles but pops open in service | Return angle too shallow, or undercut too small for the load | Steepen the return angle toward 80–90°, deepen the undercut — then re-check strain |
| Clip takes a permanent set after a few openings | Strain checked against the single-use limit, not the repeated-use limit | Apply the 60% rule for repeated use; switch away from a glass-filled grade |
| White stress marks at the root | Strain near the yield point, made worse by a sharp internal corner | Add a root fillet and reduce strain; whitening is a warning, not a cosmetic issue |
| Cover cannot be opened for service | Return angle at 90°, which makes the joint effectively permanent | Change the return angle to a serviceable range and re-check the mating force |
| Sink mark on the face opposite the clip | Arm root too thick for the wall it grows from | Thin the root or taper the arm; keep the root below about 60% of the wall thickness |
Two patterns are worth noting. First, the crack is almost always at the root, because that is where strain peaks — the arm tip barely works at all. Second, a clip that "worked in the prototype" and fails in production usually changed material, wall thickness, or gate position between prototype and production tooling, and nobody re-ran the check. The calculation in the next sections takes five minutes; the tooling change it prevents takes weeks.
Which snap-fit type fits your part?
There are four basic snap-joint forms, and choosing from the required motion — not from appearance — is the first design decision. Covestro’s design guide reduces the many possible shapes to these four, and each one bends in a different way.
| Joint type | How it bends | Best for | Releasable? | Tooling note |
|---|---|---|---|---|
| Cantilever | Beam bending | Housings, covers, panels, clips — the large majority of snap fits | Yes, by hook angle | Hook is an undercut; a through-slot under it avoids a lifter |
| U-shaped | Beam bending over a longer effective length | Lids and covers where space is short but the arm must be long | Yes | Curved or folded arm; check the bend at the U-turn |
| Annular | Multiaxial expansion around a round feature | Caps, tube fittings, lamp housings; small undercuts give strong joints | Usually single assembly | Inseparable versions need a split cavity; avoid them if you can |
| Torsion | Twisting of a bar | Rocker-style latches, instrument housings | Yes | Shear-controlled; permissible shear strain is roughly the bending strain divided by 1.35 |
The rest of this guide concentrates on the cantilever, because it covers most real applications and because it is the type you can check with a single formula. The same strain logic applies to the others: find the peak strain, compare it with what the resin tolerates, and leave margin for real life.
The one calculation that decides whether a clip survives
For a straight cantilever arm of constant rectangular section, the peak strain at the root is:
ε = 1.5 × y × h ÷ L²
- ε is the peak surface strain at the root, as a decimal (multiply by 100 for percent)
- y is the undercut depth — how far the hook tip must deflect to clear the mating edge
- h is the arm thickness at the root, in the direction of bending
- L is the free arm length, from the root to the hook
The formula comes from the Bayer and BASF snap-fit design guides, and it is the same relation used in Covestro’s Snap-Fit Joints for Plastics — A Design Guide and in Xometry Pro’s snap-fit design checker. Three things about it matter more than the algebra. First, strain falls with the square of arm length: doubling the length cuts strain to a quarter, which is why a longer arm is the most effective fix available. Second, strain rises in direct proportion to thickness, so a thinner root helps — but only until the arm becomes too weak to hold. Third, width does not appear in the formula at all: widening the arm raises assembly and retention force, but it does nothing for strain.
The allowable side of the comparison comes from the resin manufacturer, not from a rule of thumb. Covestro publishes these guide values for allowable short-term strain at 23 °C, for a single joining operation:
| Resin (Covestro grades) | Allowable short-term strain, single assembly |
|---|---|
| Makrolon polycarbonate (PC) | 4% |
| Apec high-heat PC | 4% |
| Makroblend polycarbonate | 3.5% |
| Bayblend PC/ABS | 2.5% |
| Makrolon PC, 10% glass-filled | 2.2% |
| Makrolon PC, 20% glass-filled | 2.0% |
Two rules sit on top of this table. For a joint that will be separated and rejoined repeatedly, use about 60% of the single-assembly value — for Makrolon PC, that means 2.4%, not 4%. And glass filling cuts the allowable strain roughly in half, even as it raises stiffness: the same geometry that is safe in unfilled PC can fail in a glass-filled grade. Always take the limit from the datasheet of the exact grade you will mold, at the service temperature — these published values are screening numbers for a first check, not a release criterion.
Worked example: a polycarbonate enclosure cover
Take a cover clip in Makrolon PC, single assembly, with an undercut depth of 1.2 mm and a root thickness of 2.0 mm. The allowable strain is 4%. Three versions of the same clip show how the check drives the design:
| Version | Arm length | Arm section | Peak strain | Strain used | Verdict |
|---|---|---|---|---|---|
| A — as drawn | 20 mm | Constant | ε = 1.5 × 2.0 × 1.2 ÷ 20² = 0.90% | 23% of 4% | Pass, comfortable |
| B — shortened to fit the space | 10 mm | Constant | ε = 1.5 × 2.0 × 1.2 ÷ 10² = 3.60% | 90% of 4% | Marginal for one assembly; fails repeated use |
| C — lengthened and tapered | 14 mm | Tapered to half thickness at the tip | ε = 1.2 × 2.0 ÷ (1.09 × 14²) = 1.12% | 28% of 4% | Pass, including repeated use |
The arithmetic is the point, so here it is in full. Version A: 1.5 × 2.0 × 1.2 = 3.6, divided by 20² = 400, gives 0.009, or 0.90%. Version B halves the length, and because length is squared, strain quadruples to 3.60% — 90% of the single-use limit, and 150% of the 2.4% repeated-use limit, so a serviceable cover built this way will whiten or crack within a few openings. Version C lengthens the arm to 14 mm and tapers it so the thickness falls to half at the tip; for a tapered arm the factor in the formula drops from 1.5 to 1.09, giving 2.4 ÷ (1.09 × 196) = 1.12% — 28% of the single-use limit and 47% of the repeated-use limit. Tapering is worth doing on its own: Covestro’s photoelastic comparison shows the optimal tapered arm uses 17% less material and carries 46% lower strain than a constant-section arm of the same length.
A useful screening rule follows from the same formula. Xometry Pro’s checker treats strain usage below 75% of the allowable as a comfortable pass, 75–100% as marginal — material scatter and molding variation can consume the remaining margin — and anything over 100% as exceeding the material limit. Design to the comfortable band, and treat the marginal band as a reason to change the geometry, not as a pass.
If you would rather solve for the length you need, rearrange the formula: L = √(1.5 × y × h ÷ ε-allowable). For the cover above, opened repeatedly, that gives √(3.6 ÷ 0.024) = 12.2 mm — a constant-section arm shorter than about 12 mm cannot meet the repeated-use limit at all, whatever else you change.
How much force will assembly and removal take?
A snap fit has to satisfy two people at once: the assembler who pushes it together, and the user who must not pull it apart by accident. The two forces come from the same deflection force, shaped by the hook angles and by friction — and the asymmetry is the whole point of the design.
The deflection force P is the force needed to bend the arm by the undercut depth. The mating force W — what the assembler actually feels — is larger, because the hook face is a wedge sliding against the mating edge:
W = P × (μ + tan α) ÷ (1 − μ × tan α)
Here α is the entry angle of the hook face and μ is the friction coefficient between the two materials. A shallow entry angle, typically 30°, keeps assembly force low. The return angle decides what happens afterwards: around 80° the joint is serviceable but firm, and at 90° it becomes effectively permanent, because the pull-off force rises beyond what the parts can transmit without breaking.
Covestro’s own worked example makes the numbers concrete. A Makrolon PC hook 19 mm long, 9.5 mm wide, with a 2.4 mm undercut and a 30° entry angle, needs a deflection force of 32.5 N. Against the same material, with a friction coefficient of 0.6, the mating force is 58.5 N — nearly twice the deflection force, because of the wedge and the friction. That is the force your assembler feels, and it is the number to compare with what a hand assembly operation can comfortably deliver.
Friction is not a minor term. Covestro’s Table 3 gives these coefficients for plastics sliding on steel:
| Material pair (on steel) | Friction coefficient μ |
|---|---|
| PTFE | 0.12–0.22 |
| PP | 0.25–0.30 |
| POM | 0.20–0.35 |
| PA | 0.30–0.40 |
| PC | 0.45–0.55 |
| ABS | 0.50–0.65 |
Two mating parts of the same plastic rub harder than plastic on steel — Covestro applies a factor of about 1.2 for PC and ABS pairs — so a PC clip snapping into a PC housing sees more friction than the steel-column values suggest. If assembly force is a problem, the levers are the entry angle, the undercut depth, and the material pairing, in that order; changing the resin to cut friction is usually the last resort, because it changes the strain limit too.
What does the snap fit cost in the mold?
A snap fit is cheap as a feature and expensive as a tooling decision, and the difference is the undercut. The hook must catch behind a ledge, which means some part of the mold has to form a face the part cannot simply slide off. There are two ways to do it, and the quote will show the difference.
The low-cost route is a through-slot in the wall directly beneath the hook. A straight-pull core passes through the slot to form the undercut face, the mold opens without any moving mechanism, and the slot doubles as a shutoff surface. The higher-cost route is a lifter or a side action, which the tool needs when the hook sits on a solid wall with no slot behind it. If your supplier’s quote includes a lifter for every clip, ask whether a slot would do the job — it is the single most common cost-saving detail in snap-fit design.
Three more mold details decide whether the clip molds cleanly. First, draft: at least 0.5° per side on the arm faces, so the arm releases without dragging. Second, ejection: place ejector pins near the root, never on the flexing arm, so no witness mark lands on the highest-stress region. Third, the root thickness: if the arm root is much thicker than the wall it grows from — roughly above 60% of the wall thickness — expect a sink mark on the opposite face, and a thick section at the root also traps residual stress. A generous root fillet helps twice: it spreads the stress concentration, and it avoids the sharp corner where cracks start. Covestro notes the stress-concentration benefit flattens out around a radius-to-thickness ratio of 0.6, but a large radius also creates the thick section that causes sinks — the practical compromise is a radius of about 0.4 times the root thickness, and never below 0.38 mm (0.015 in).
Gate placement matters too, for a reason that does not show up in the strain formula. If the gate puts a weld line — the line where two flow fronts meet — across the flexing arm, the arm is weakest exactly where it bends most. Ask where the gate will sit and where the weld lines will fall, and keep them off the arm. The same question belongs in a DFM review, and it is one of the checks worth running before steel is cut.
How do you prove the snap fit before production?
A snap fit is proven by assembling it, not by looking at it. Before the first production run, agree with your supplier what evidence the first articles must carry — and agree it before T1, when changes are still cheap.
- Assembly cycles. State how many times the joint will be assembled and disassembled in service, and ask the supplier to run that many cycles on first articles and report any whitening, cracking, or loss of retention. A cover opened weekly and a cover opened once at installation need very different evidence.
- Retention check. State the pull-off or push-out load the joint must resist in service, and ask for the measured result on first articles — not a calculation, a measurement.
- Visual inspection. Check the root of every first-article arm for stress whitening, hairline cracks, and sink marks on the opposite face. Whitening at the root means the strain is near the yield point, even if the clip has not cracked yet.
- Dimensions that matter. Measure the undercut depth, the arm thickness at the root, and the arm length on first articles. These three numbers are the inputs to the strain check; if they drift from the drawing, the check you ran no longer describes the part you received.
- Molded in the production resin. A snap fit validated in a prototype resin or a 3D-printed material proves nothing about the production part. First-article evidence must come from parts molded in the production grade, on the production tool.
If any of these checks fail, the fixes are the ones in the table above, in this order: lengthen the arm, taper it, reduce the undercut, change the hook angles, and only then change the resin. Changing the resin first is the most expensive way to fix a geometry problem.
What to put in your RFQ
A snap fit that is specified properly is a short list, not a long one. Send your supplier:
- The joint type and whether it must be permanent, serviceable, or repeatedly removable
- The resin grade, and the allowable strain from that grade’s datasheet at the service temperature
- The arm dimensions: length, root thickness, undercut depth, entry and return angles
- The number of assembly cycles the joint must survive, and the retention load it must hold
- Whether a through-slot is acceptable in the wall behind the hook, or whether the design needs a lifter
- The first-article evidence you expect: cycle test, retention measurement, root inspection, and the three dimensions above
If you are still deciding between a snap fit and another way of joining the parts, read our comparison of ultrasonic welding, adhesive bonding, and mechanical fastening — a snap fit is the fourth option, and it is the right one when the joint must be tool-free, fast to assemble, and cheap at volume. Snap fits also pair naturally with living hinges in enclosures and caps, where one molded part provides both the flexing hinge and the latch; the hinge carries the repeated bending, and the clip carries the retention, so check both features against their own strain limits. And because the undercut depth and arm thickness are dimensions, the tolerances your drawing can realistically hold decide how much margin the strain check needs — a tight undercut tolerance is worth paying for on a clip that sits near its strain limit.
FAQ
Can I use a glass-filled resin for a snap fit?
Only with extreme caution, and only after re-running the strain check with the filled grade’s lower allowable strain. Glass filling raises stiffness but cuts the strain the material tolerates — for polycarbonate, Covestro’s guide values fall from 4% unfilled to 2.2% at 10% glass and 2.0% at 20% glass. The same geometry that passes comfortably unfilled can exceed the limit when filled. If the part needs the stiffness of a filled grade, make the arm longer and taper it, and validate with first-article cycle testing.
Why did my clip work in the prototype and crack in production?
The most common reasons are a change of resin grade, a change of wall or arm thickness between prototype and production tooling, or a weld line landing on the arm in the production gate layout. Any of the three changes the strain the arm actually sees. Re-run the strain check against the production drawing and the production resin, and check the first articles for whitening at the root — it appears before the crack does.
How many times can a snap fit be opened and closed?
It depends on the strain the arm sees on every cycle, compared with the repeated-use limit — about 60% of the single-assembly allowable strain. A clip running at 30% of the single-use limit has a large margin for repeated use; a clip running at 90% may survive one assembly and fail on the fifth opening. The honest answer is a test: agree a cycle count with your supplier, run it on first articles, and inspect the roots.
The next step
A snap fit is one of the cheapest joints in injection molding — and one of the easiest to get wrong by skipping a five-minute check. Size the arm against the resin’s allowable strain, set the hook angles for the service life you need, and ask for first-article evidence that the clip survives the cycles it will see in the real product.
If you have a housing, cover, or enclosure that needs a snap-fit latch, send us the STEP file or 2D drawing with the material, the number of assembly cycles, the retention load, and the quantities. We will review the clip geometry against the strain check above and quote the part and the tool together — request a quote or contact us with your drawing.